Vacuum Pump Accessories - Essential Components

All Categories

vacuum pump accessories

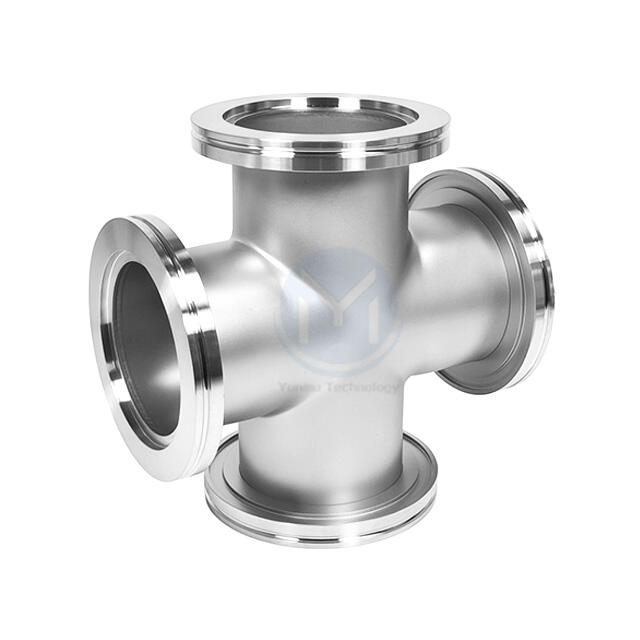
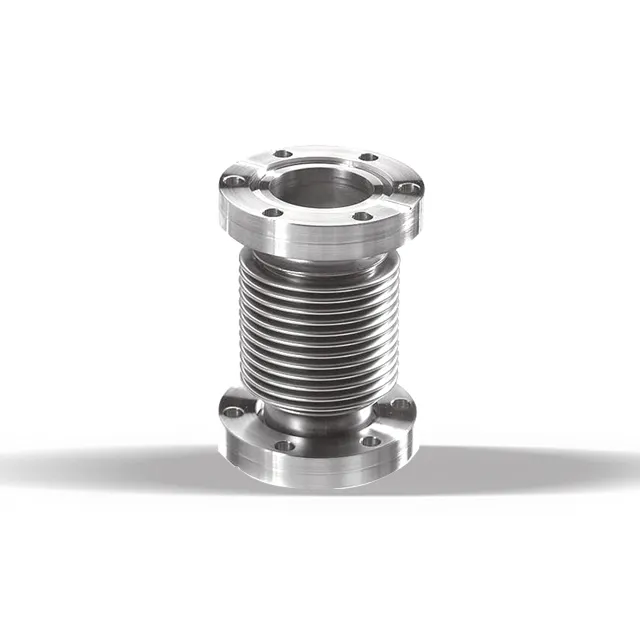
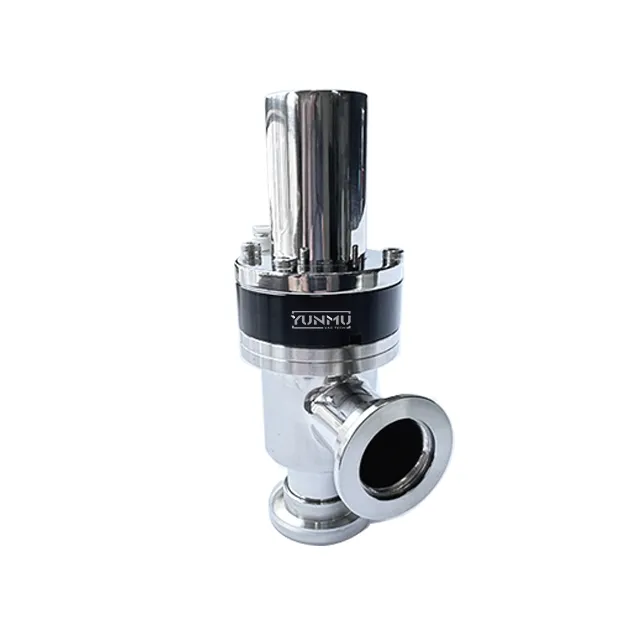
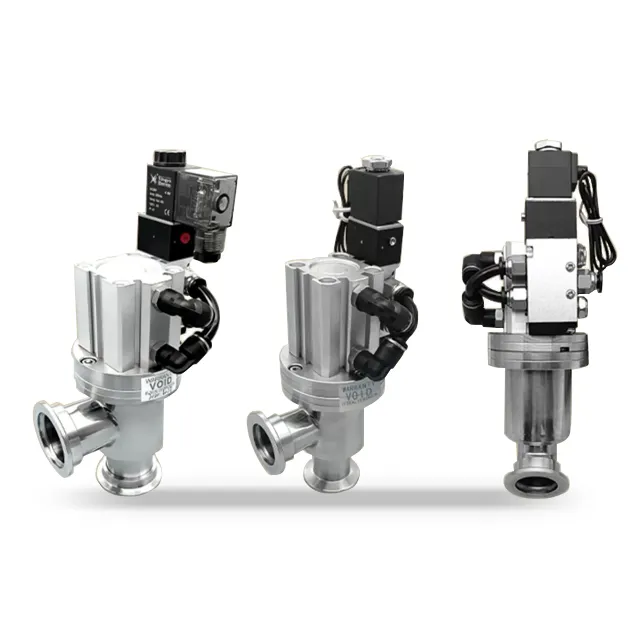
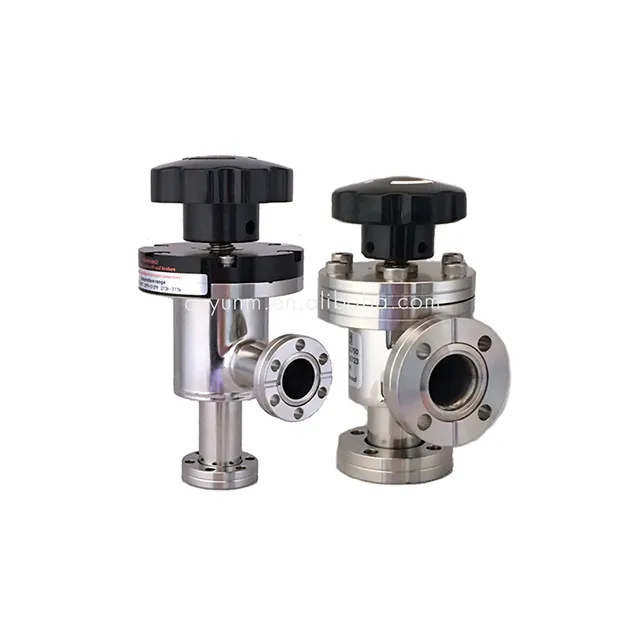
Vacuum pump accessories are essential components designed to enhance the performance, efficiency, and longevity of vacuum systems across diverse industrial applications. These accessories include a comprehensive range of products such as oil mist filters, exhaust filters, intake filters, sight glasses, oil drain valves, coupling guards, and pressure gauges. Each accessory serves a specific purpose in maintaining optimal vacuum pump operation while reducing maintenance costs and extending equipment lifespan. Modern vacuum pump accessories incorporate advanced materials and precision engineering to withstand demanding operating conditions, including extreme temperatures, corrosive environments, and continuous duty cycles. These components work synergistically with vacuum pumps to improve system reliability, protect against contamination, and ensure consistent vacuum levels. Quality vacuum pump accessories are manufactured to meet stringent industry standards and undergo rigorous testing to guarantee compatibility with various pump models and brands. From oil-sealed rotary vane pumps to dry screw pumps, appropriate accessories are available for every vacuum technology. Proper selection and installation of vacuum pump accessories directly impact system efficiency, energy consumption, and operational safety. Industries ranging from semiconductor manufacturing and pharmaceutical production to food packaging and automotive applications rely on these critical components to maintain process integrity and product quality. Understanding the role of each accessory helps operators make informed decisions about system configuration, preventive maintenance schedules, and upgrade opportunities that deliver measurable return on investment.

New Products

Investing in quality vacuum pump accessories delivers substantial cost savings through reduced downtime and extended pump service life. When properly maintained with appropriate accessories, vacuum systems operate more efficiently, consuming less energy while delivering consistent performance. Oil mist filters and exhaust filters prevent environmental contamination and protect workplace air quality, ensuring compliance with health and safety regulations while creating a cleaner production environment. These protective components also prevent oil carryover into process chambers, eliminating product defects and costly rework. Sight glasses enable operators to monitor oil condition and levels without interrupting operations, facilitating proactive maintenance that prevents catastrophic failures. Pressure gauges provide real-time system monitoring, allowing immediate detection of performance degradation or potential issues before they escalate into expensive repairs. Intake filters protect internal pump components from particulate contamination that causes premature wear, significantly extending intervals between major overhauls. Coupling guards enhance operator safety by preventing contact with rotating components while allowing easy inspection and alignment verification. Quick-connect fittings and drain valves simplify routine maintenance tasks, reducing service time and associated labor costs. The modularity of vacuum pump accessories allows system customization to meet specific application requirements without replacing entire pumps. This flexibility enables businesses to adapt existing equipment to new processes or production demands cost-effectively. Quality accessories maintain optimal sealing and minimize leak paths, preserving vacuum integrity and process repeatability. By preventing system contamination and maintaining clean operating conditions, these accessories reduce the frequency of costly pump rebuilds and component replacements. The cumulative effect of properly selected vacuum pump accessories translates to improved productivity, lower total cost of ownership, and enhanced operational reliability that directly supports business profitability and competitive advantage in demanding manufacturing environments.

Tips And Tricks

How Does a Vacuum Chamber Support High Precision Manufacturing?

29

May

How Does a Vacuum Chamber Support High Precision Manufacturing?

In high precision manufacturing, even the smallest environmental variable can compromise the integrity of a finished component. Contaminants in the air, fluctuating pressure, and trace moisture are invisible threats that can distort measurements, wea...
View More
How Do Custom Vacuum Systems Support Specialized Manufacturing Needs?

29

May

How Do Custom Vacuum Systems Support Specialized Manufacturing Needs?

In today's advanced manufacturing landscape, standard off-the-shelf equipment often falls short when processes demand precision, repeatability, and environmental control that generic solutions simply cannot deliver. custom vacuum systems have emerged...
View More
Why Are Integrated Vacuum Solutions Important for Modern Factories?

04

Jun

Why Are Integrated Vacuum Solutions Important for Modern Factories?

Modern manufacturing environments are under constant pressure to improve efficiency, reduce contamination risks, and maintain precise process control across every production stage. In this context, vacuum solutions have evolved from being a periphera...
View More
How Can Edge Welded Bellow Systems Improve Vacuum Performance?

04

Jun

How Can Edge Welded Bellow Systems Improve Vacuum Performance?

In high-precision vacuum environments, even the smallest mechanical compromise can lead to significant performance degradation. The edge welded bellow has emerged as one of the most reliable solutions for maintaining vacuum integrity while accommodat...
View More

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

vacuum pump accessories

Superior Filtration Technology

Superior Filtration Technology

Modern vacuum pump accessories incorporate advanced filtration technology that protects both equipment and environment from harmful contaminants. High-efficiency oil mist filters capture microscopic oil droplets before they enter the atmosphere, achieving separation efficiencies exceeding 99.9 percent while maintaining minimal backpressure. These sophisticated filters utilize multi-stage separation mechanisms combining coalescence, impaction, and diffusion to remove particles as small as 0.01 microns. The filtration media in premium vacuum pump accessories resists saturation and maintains consistent performance throughout extended service intervals, reducing replacement frequency and associated maintenance costs. Exhaust filters prevent oil vapor from contaminating cleanrooms and production areas, critical for industries with strict environmental controls. Intake filters employ pleated designs that maximize surface area within compact housings, extending service life while protecting pump internals from abrasive particles that cause wear. Advanced filter designs incorporate drainage systems that automatically return captured oil to the pump reservoir, reducing oil consumption and operating costs. Replaceable filter elements simplify maintenance while allowing users to upgrade filtration performance without modifying system infrastructure. The superior filtration capabilities of quality vacuum pump accessories ensure compliance with environmental regulations, protect product quality, and create safer working conditions while extending pump operational life.
Precision Monitoring Components

Precision Monitoring Components

Accurate system monitoring through specialized vacuum pump accessories enables proactive maintenance strategies that prevent unexpected failures and optimize performance. Digital and analog pressure gauges provide real-time vacuum level indication with accuracy tolerances within one percent of full scale, allowing operators to detect subtle performance changes before they impact production. Illuminated sight glasses with temperature-resistant materials enable visual oil condition assessment even in poorly lit environments, revealing contamination, degradation, or inadequate lubrication levels at a glance. Advanced monitoring accessories include electronic sensors that integrate with automated control systems, providing continuous data logging and alarm functionality for unmanned operations. These precision instruments help establish performance baselines and track degradation trends over time, supporting predictive maintenance programs that schedule service based on actual condition rather than arbitrary intervals. Temperature gauges monitor thermal conditions that indicate bearing wear, inadequate cooling, or excessive ambient temperatures affecting pump efficiency. Vibration sensors detect imbalance or mechanical issues in early stages when corrective action is simple and inexpensive. The diagnostic capabilities provided by monitoring vacuum pump accessories transform maintenance from reactive crisis management to strategic asset management, reducing emergency repairs and maximizing equipment availability for production demands.
Enhanced Safety and Convenience Features

Enhanced Safety and Convenience Features

Safety-focused vacuum pump accessories protect personnel while simplifying routine maintenance procedures that keep systems operating reliably. Coupling guards manufactured from impact-resistant transparent materials provide complete protection from rotating shafts while allowing visual inspection of alignment and coupling condition without disassembly. These guards incorporate interlocked access panels that automatically shut down equipment when opened, preventing accidental contact during service. Quick-disconnect fittings with automatic shutoff valves enable tool-free oil changes and filter replacements, reducing maintenance time while eliminating spills that create slip hazards and environmental concerns. Thermally insulated exhaust components prevent burn injuries from hot discharge lines while improving energy efficiency through heat recovery opportunities. Anti-vibration mounting accessories reduce noise transmission and structural stress, creating quieter work environments and extending building infrastructure life. Ergonomically designed drain valves position at convenient heights with large handles operable while wearing protective gloves, accommodating real-world working conditions. Safety relief valves protect against overpressure conditions that could damage equipment or create hazardous situations. Standardized connections across vacuum pump accessories families ensure compatibility and reduce inventory complexity while preventing incorrect installations. These thoughtful design features demonstrate how quality accessories enhance workplace safety and operational convenience simultaneously.

Have questions about the company?

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000