Vacuum Technology Manufacturer Solutions

All Categories

vacuum technology manufacturer

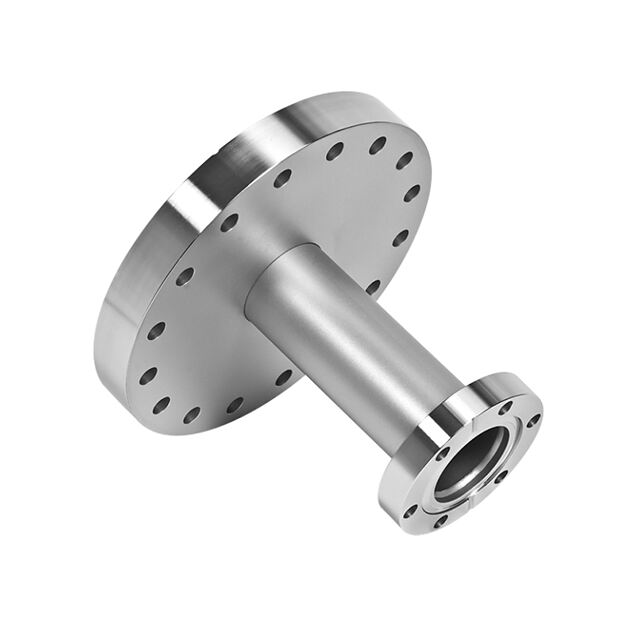
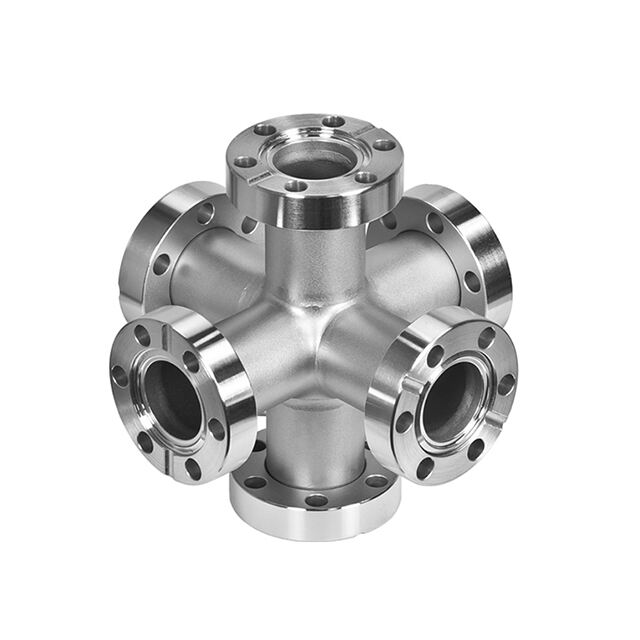
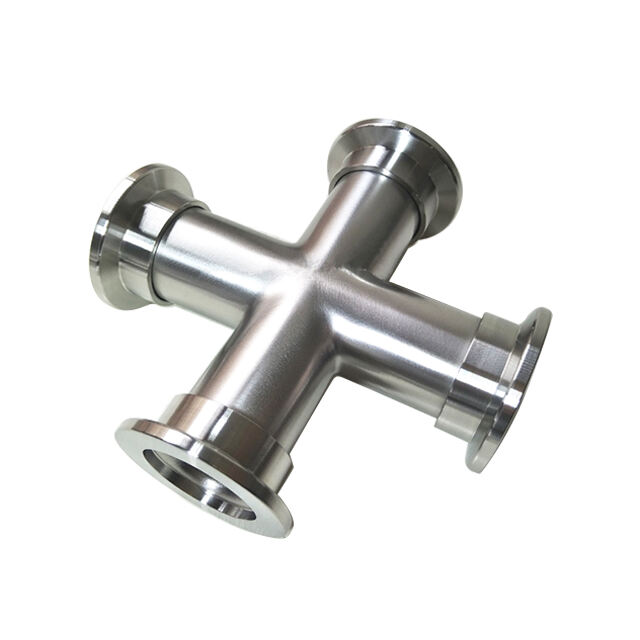
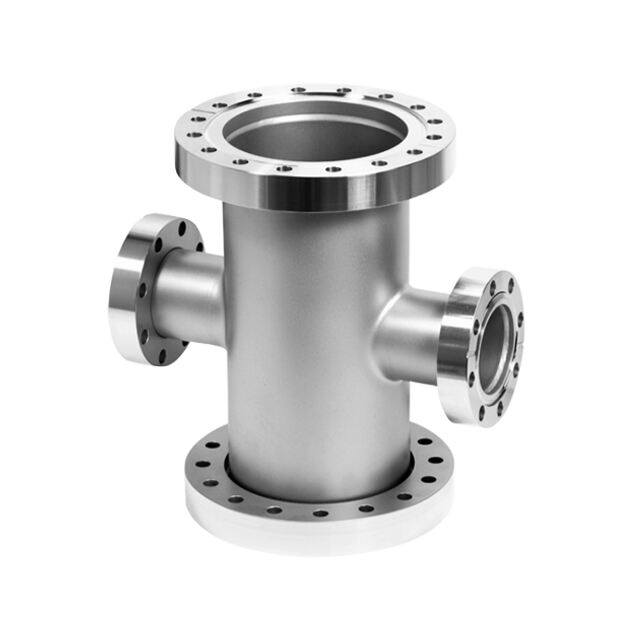
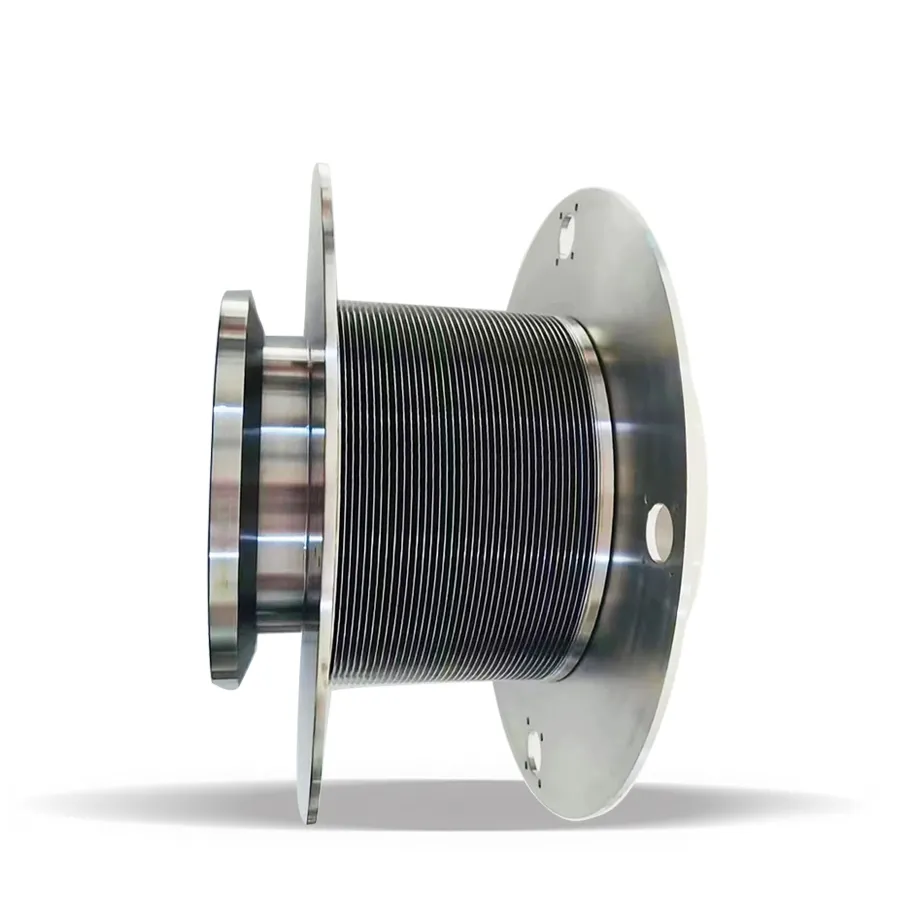
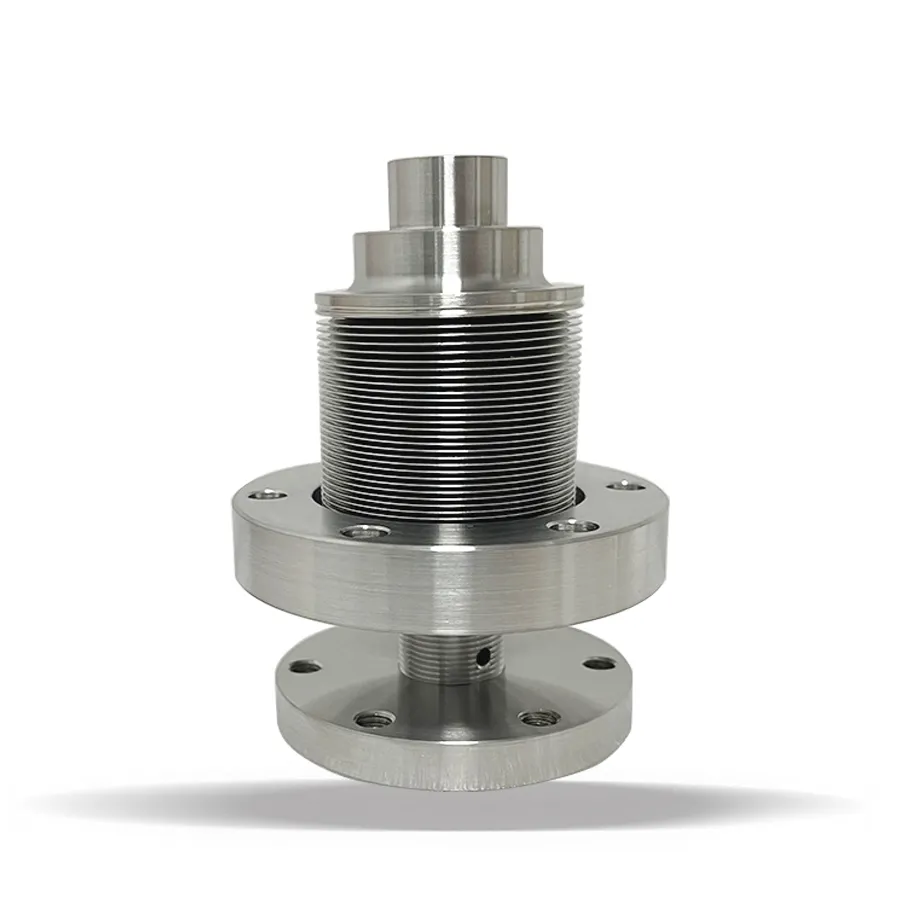
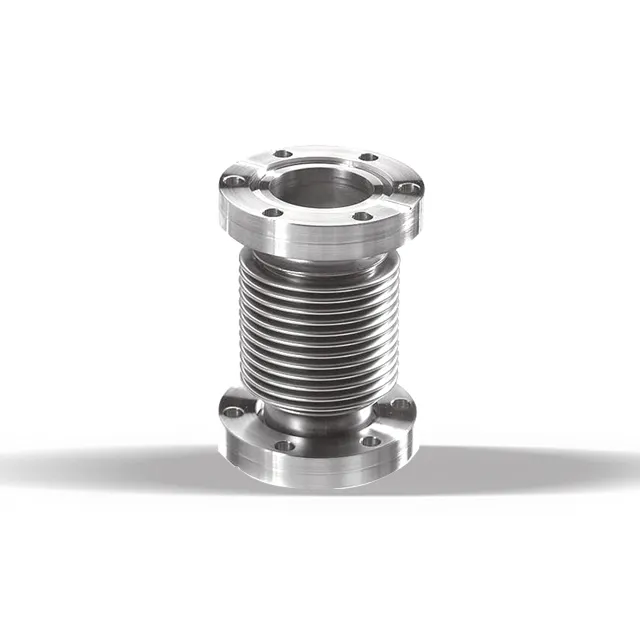
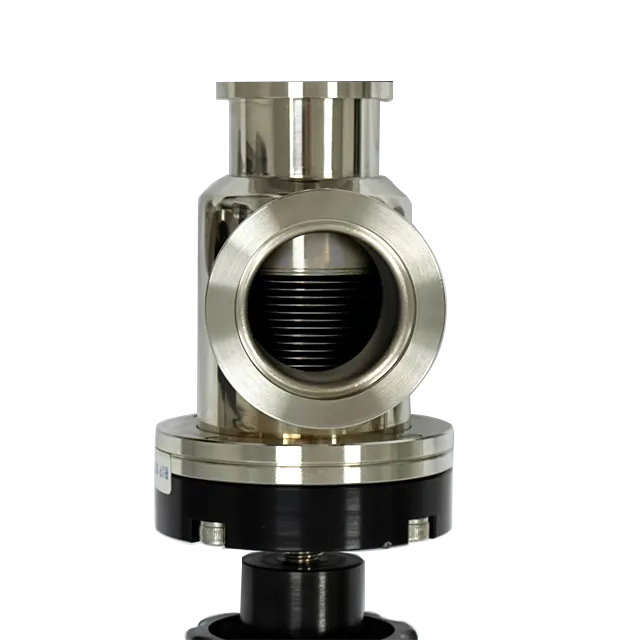
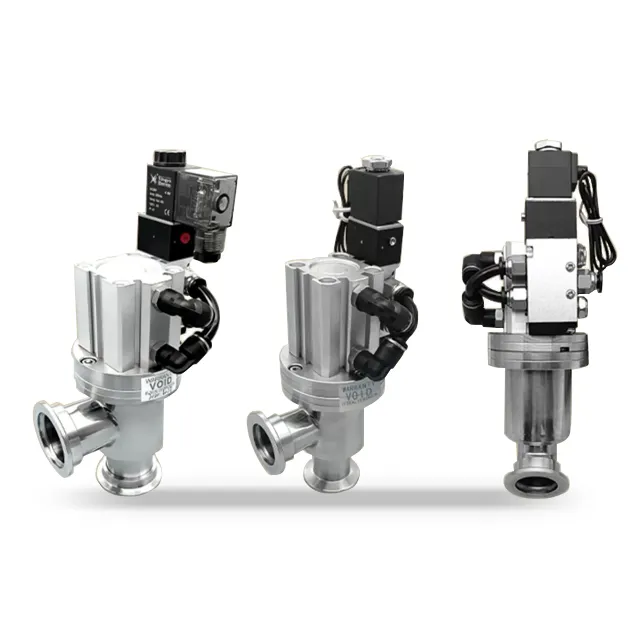
A vacuum technology manufacturer specializes in designing, producing, and supplying advanced vacuum systems and components that create low-pressure environments for industrial and scientific applications. These manufacturers develop a comprehensive range of products including vacuum pumps, chambers, valves, gauges, and complete integrated systems that remove air and gases from sealed spaces. The main functions encompass achieving varying vacuum levels from rough vacuum to ultra-high vacuum conditions, maintaining consistent pressure control, and ensuring contamination-free environments essential for sensitive processes. Technologically, a vacuum technology manufacturer incorporates precision engineering with materials resistant to corrosion and outgassing, implements sophisticated sealing mechanisms, and integrates digital monitoring systems for real-time performance tracking. Modern vacuum systems feature energy-efficient motor designs, automated control interfaces, and modular configurations that allow customization based on specific operational requirements. Applications span numerous industries including semiconductor fabrication where ultra-clean environments prevent particle contamination, pharmaceutical production requiring sterile processing conditions, food packaging that extends shelf life through oxygen removal, metallurgy for heat treatment processes, and research laboratories conducting experiments under controlled atmospheric conditions. A vacuum technology manufacturer serves critical roles in coating technologies, electron microscopy, mass spectrometry, and aerospace testing facilities. The versatility of vacuum systems makes them indispensable across manufacturing sectors where precise environmental control directly impacts product quality and process efficiency.

New Product Releases

Choosing the right vacuum technology manufacturer delivers substantial operational and financial benefits that directly impact your production capabilities and bottom line. Quality manufacturers provide reliable equipment that minimizes downtime through robust construction and proven designs, ensuring your operations maintain consistent productivity without unexpected interruptions. You gain access to systems engineered for energy efficiency, reducing operational costs significantly compared to outdated technologies while meeting environmental sustainability goals. A reputable vacuum technology manufacturer offers comprehensive technical support and maintenance services, providing peace of mind through expert guidance during installation, training, and ongoing operations. This partnership approach means faster problem resolution and optimized system performance tailored to your specific applications. You benefit from scalable solutions that grow with your business needs, allowing incremental capacity expansion without complete system replacement. The flexibility of working with an experienced vacuum technology manufacturer means receiving customized configurations that address unique process requirements rather than settling for generic off-the-shelf products. Advanced monitoring capabilities integrated into modern vacuum systems provide actionable data insights, enabling predictive maintenance that prevents costly failures and extends equipment lifespan. You achieve superior process control that translates directly into improved product quality, reduced waste rates, and enhanced yield in critical manufacturing operations. Manufacturers with extensive industry experience bring valuable application knowledge, helping you identify optimal vacuum solutions that maximize return on investment. The right vacuum technology manufacturer maintains rigorous quality standards and certifications, ensuring compliance with industry regulations and international safety requirements. This reduces your risk exposure and simplifies auditing processes while guaranteeing equipment reliability under demanding operational conditions.

Latest News

How Can Vacuum Technology Improve Process Stability and Output?

29

May

How Can Vacuum Technology Improve Process Stability and Output?

In modern industrial manufacturing, process stability and consistent output are not optional goals — they are operational necessities. vacuum technology has emerged as one of the most reliable engineering tools for achieving both. By removing gas mol...
View More
Why Are Stainless Steel Vacuum Fittings Preferred in Harsh Environments?

29

May

Why Are Stainless Steel Vacuum Fittings Preferred in Harsh Environments?

In industrial and scientific settings where reliability is non-negotiable, the choice of vacuum fittings can determine whether a system performs flawlessly or fails under pressure. Stainless steel has emerged as the dominant material for vacuum fitti...
View More
Why Is Vacuum Chamber Design Important for Industrial Applications?

29

May

Why Is Vacuum Chamber Design Important for Industrial Applications?

In industrial manufacturing and research environments, the vacuum chamber is far more than a sealed metal enclosure. It is a precisely engineered system whose design directly determines whether a process succeeds or fails. From semiconductor fabricat...
View More
Why Are Integrated Vacuum Solutions Important for Modern Factories?

04

Jun

Why Are Integrated Vacuum Solutions Important for Modern Factories?

Modern manufacturing environments are under constant pressure to improve efficiency, reduce contamination risks, and maintain precise process control across every production stage. In this context, vacuum solutions have evolved from being a periphera...
View More

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

vacuum technology manufacturer

Precision Engineering Excellence

Precision Engineering Excellence

A leading vacuum technology manufacturer distinguishes itself through exceptional precision engineering that delivers consistent performance across demanding applications. Every component undergoes rigorous quality control testing to ensure dimensional accuracy, material integrity, and functional reliability before reaching customers. This meticulous approach guarantees vacuum systems maintain specified pressure levels with minimal fluctuation, critical for processes requiring stable environmental conditions. Advanced manufacturing techniques including CNC machining, laser welding, and automated assembly ensure repeatable quality across production runs. The engineering excellence extends to material selection, where manufacturers utilize specialized alloys, ceramics, and elastomers chosen specifically for their vacuum compatibility, outgassing properties, and durability under extreme conditions. Precision-manufactured sealing surfaces eliminate leak paths that compromise vacuum integrity, while carefully balanced rotating assemblies in pumps minimize vibration and wear. This attention to engineering detail translates into longer service intervals, reduced maintenance requirements, and lower total cost of ownership. Customers investing in equipment from a vacuum technology manufacturer committed to precision engineering experience fewer operational disruptions and achieve tighter process tolerances, directly enhancing their competitive positioning in quality-sensitive markets.
Comprehensive Application Support

Comprehensive Application Support

An exceptional vacuum technology manufacturer provides comprehensive application support that extends far beyond equipment delivery, serving as a strategic partner throughout your project lifecycle. Expert applications engineers collaborate with customers during the planning phase, analyzing process requirements, environmental constraints, and performance objectives to recommend optimal vacuum solutions. This consultative approach prevents costly specification errors and ensures system capabilities align precisely with operational needs. Support continues through installation with on-site commissioning services that verify proper setup, optimize parameters, and train operators on best practices for equipment operation and routine maintenance. A dedicated vacuum technology manufacturer maintains technical support teams with deep product knowledge and troubleshooting expertise, providing rapid response when questions arise or assistance is needed. Documentation packages include detailed operation manuals, maintenance schedules, and spare parts lists that simplify ongoing system management. Many manufacturers offer performance monitoring services and periodic system audits to identify optimization opportunities before efficiency degradation impacts production. This proactive support philosophy helps customers maximize equipment utilization rates and extend operational lifespan. Access to application laboratories for process testing and validation provides additional confidence when implementing new vacuum processes, reducing implementation risks and accelerating time-to-production.
Innovation and Technology Leadership

Innovation and Technology Leadership

A forward-thinking vacuum technology manufacturer invests continuously in research and development, driving innovation that keeps customers at the forefront of industry capabilities. Technology leadership manifests through integration of Industry 4.0 concepts including IoT connectivity, cloud-based monitoring platforms, and predictive analytics that transform vacuum systems into intelligent assets. Smart sensors embedded throughout vacuum equipment collect operational data, enabling remote diagnostics and condition-based maintenance strategies that minimize unplanned downtime. Manufacturers pioneering new pump designs achieve higher efficiencies, lower noise levels, and reduced energy consumption compared to conventional technologies, delivering measurable operational savings. Innovations in materials science result in components with superior chemical resistance, extended service life, and enhanced performance under extreme temperatures. A progressive vacuum technology manufacturer actively collaborates with research institutions and industry partners, ensuring products incorporate latest scientific advances and address emerging application challenges. Customers benefit from access to cutting-edge solutions that provide competitive advantages through improved process capabilities, faster cycle times, and enhanced product quality. Technology leadership also encompasses environmental responsibility, with manufacturers developing oil-free pumps, refrigerant-free cooling systems, and energy recovery features that reduce environmental footprint while lowering operating costs. Choosing an innovative manufacturer ensures your vacuum infrastructure remains technologically relevant and operationally optimized.

Have questions about the company?

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000