Ultra High Vacuum Solutions | Advanced Systems

All Categories

ultra high vacuum solutions

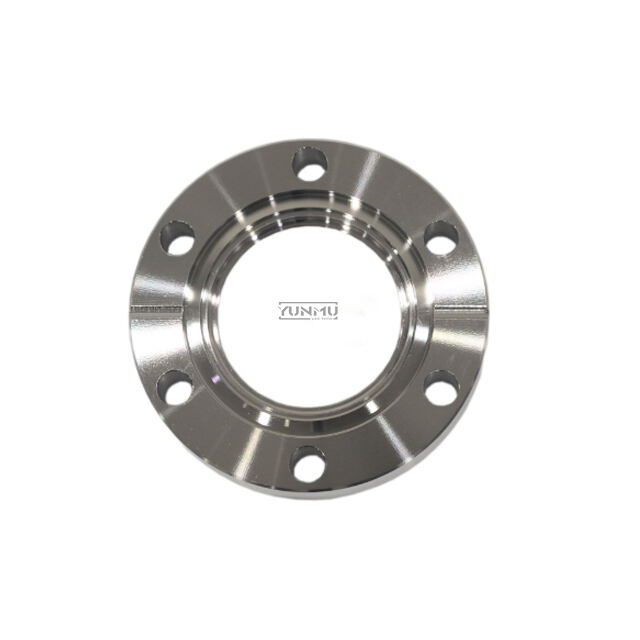
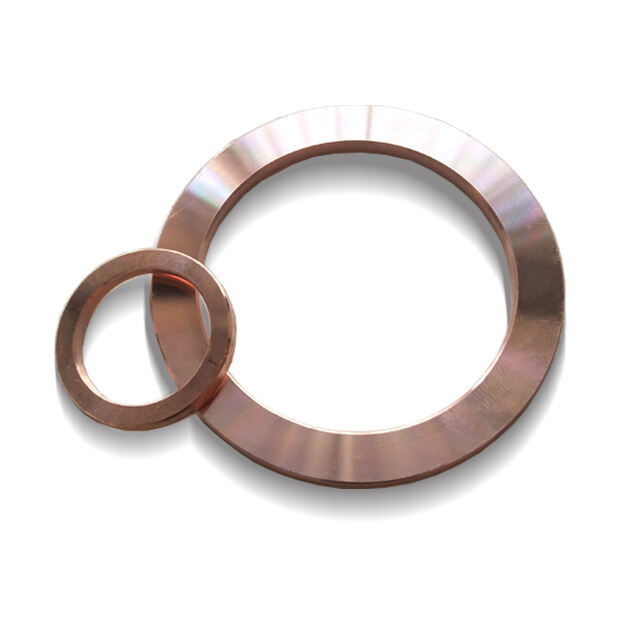
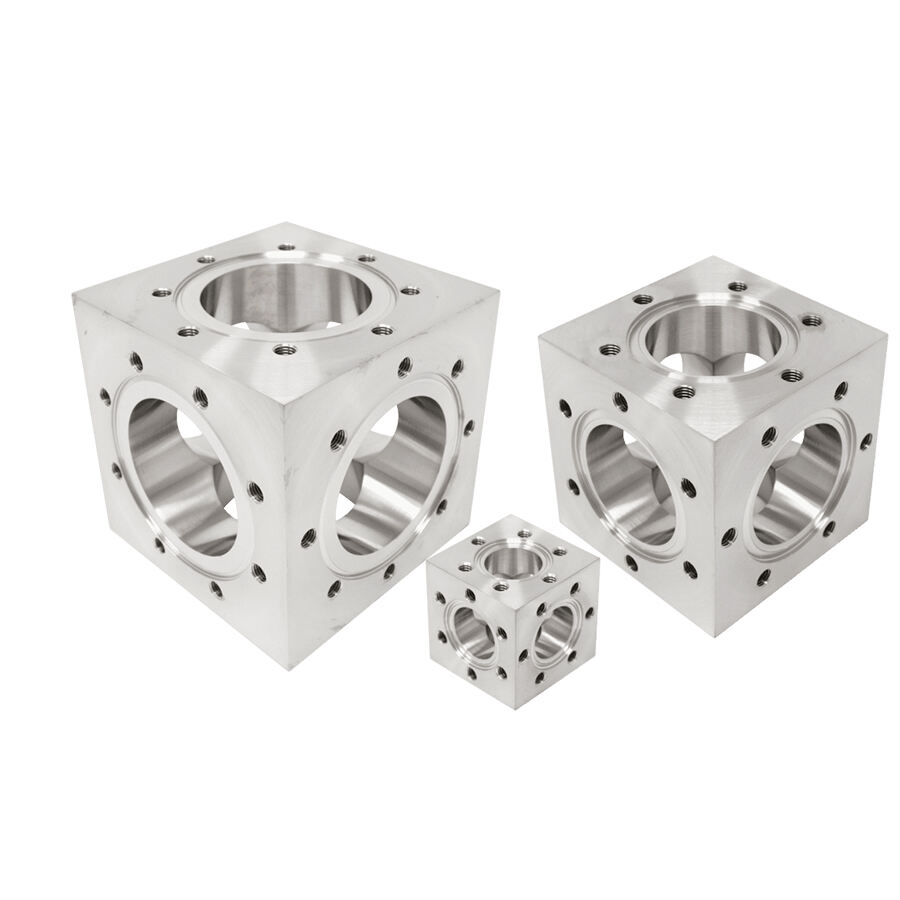
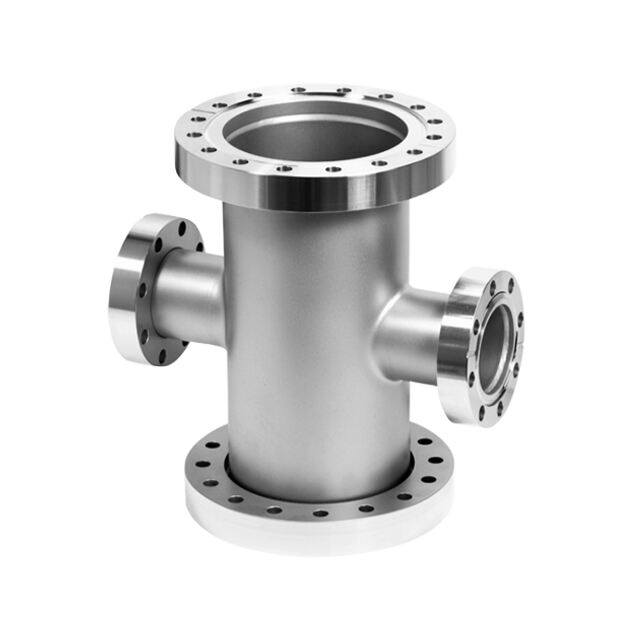
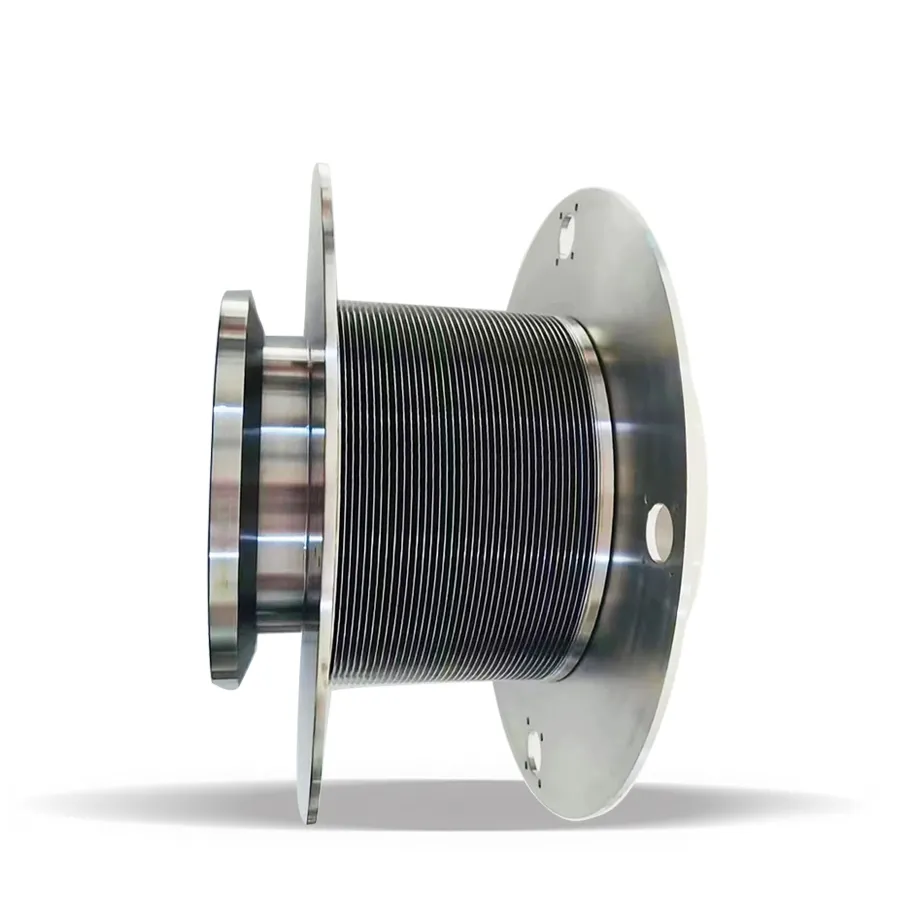
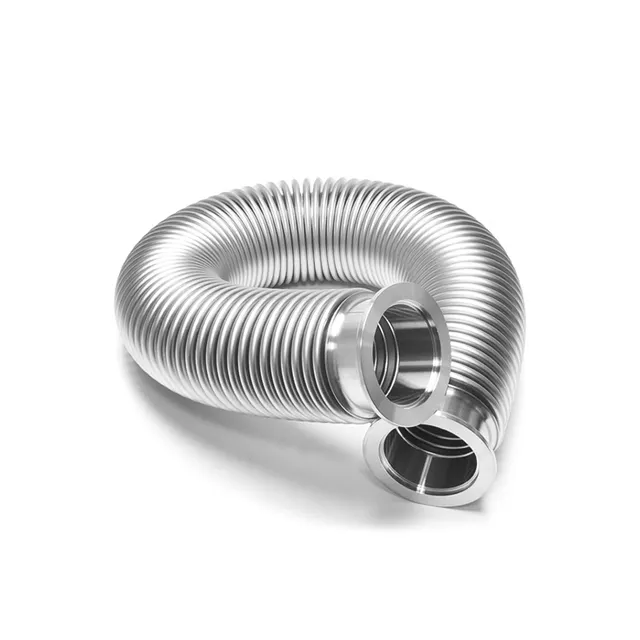
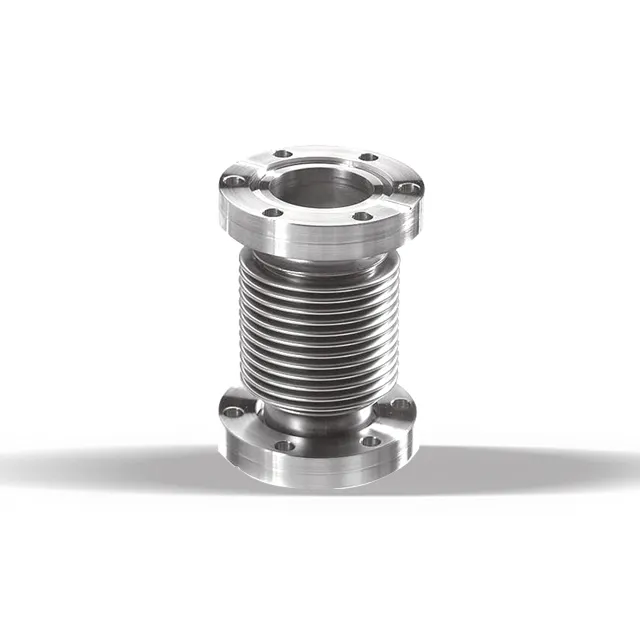
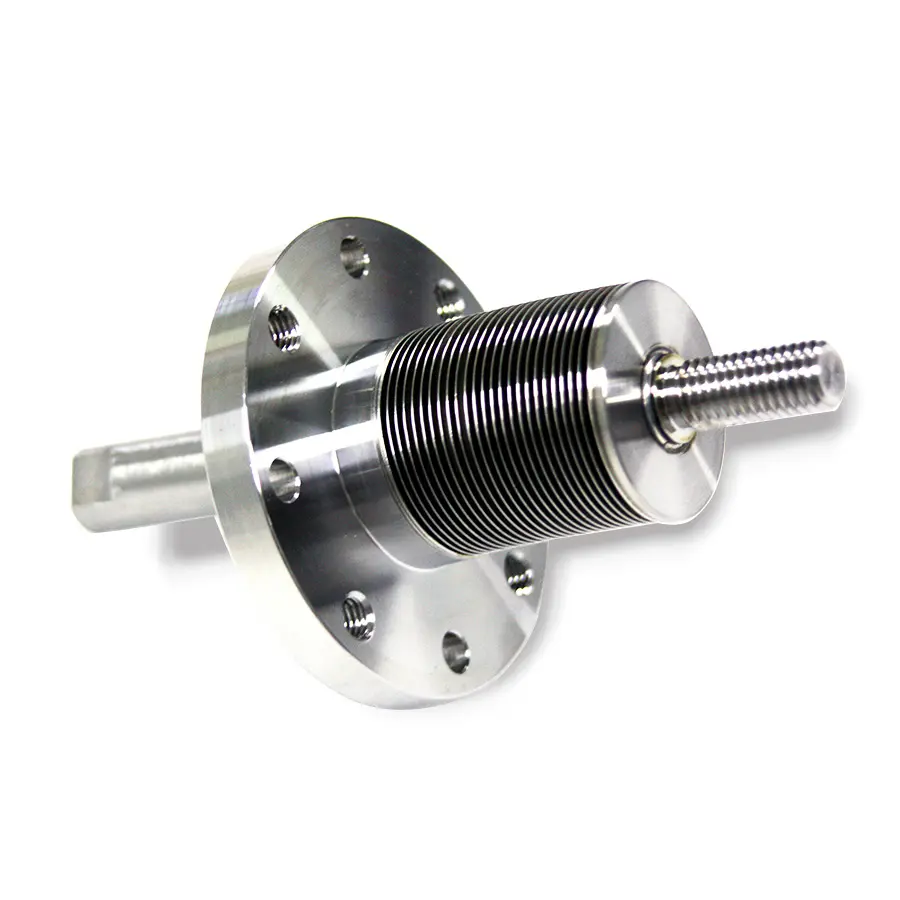
Ultra high vacuum solutions represent advanced technological systems designed to create and maintain extremely low-pressure environments, typically below 10^-9 mbar. These sophisticated solutions are essential for applications requiring contaminant-free conditions and precise control over atmospheric composition. The main functions include achieving exceptional vacuum levels, maintaining pressure stability over extended periods, and providing reliable contamination control. Ultra high vacuum solutions incorporate cutting-edge pumping technologies such as ion pumps, turbomolecular pumps, and titanium sublimation pumps working in coordinated sequences. The technological features encompass leak-tight chamber construction using stainless steel or aluminum alloys, precision-engineered sealing mechanisms with metal gaskets, comprehensive pressure monitoring through ionization gauges, and automated control systems that optimize pumping sequences. These solutions integrate bakeout capabilities to remove residual gases from internal surfaces, ensuring superior vacuum quality. Applications span diverse industries including semiconductor manufacturing where wafer processing demands particle-free environments, surface science research requiring pristine sample analysis, thin-film deposition for optical coatings and electronic components, mass spectrometry laboratories conducting molecular analysis, and particle accelerator facilities. Ultra high vacuum solutions also serve aerospace testing, materials research, and nanotechnology development where atomic-level precision is mandatory. The combination of robust engineering, intelligent automation, and proven reliability makes these systems indispensable for organizations pursuing excellence in high-tech manufacturing, scientific research, and quality-critical production processes.

Popular Products

Investing in ultra high vacuum solutions delivers substantial operational advantages that directly impact your bottom line and competitive positioning. These systems dramatically reduce contamination risks, ensuring product quality remains consistently high throughout manufacturing cycles. When production batches meet specifications without defects caused by atmospheric contaminants, you save significant costs on waste, rework, and customer returns. The enhanced process control enables precise manipulation of deposition rates, reaction conditions, and material properties, translating into superior product performance and differentiation in demanding markets. Energy efficiency represents another practical benefit, as modern ultra high vacuum solutions incorporate intelligent pumping strategies that minimize power consumption while maintaining optimal pressure levels. This reduces operational expenses over the equipment lifecycle. Reliability is paramount in production environments, and these solutions are engineered for continuous operation with minimal downtime, protecting your production schedules and delivery commitments. The automation features reduce labor requirements for routine monitoring and adjustments, freeing skilled personnel for higher-value tasks. Ultra high vacuum solutions offer excellent scalability, accommodating future capacity expansion or process modifications without requiring complete system replacement. The compatibility with various chamber sizes and configurations means these solutions adapt to your specific application requirements rather than forcing compromise. For research organizations, the capability to achieve and maintain extreme vacuum levels opens possibilities for groundbreaking experiments and discoveries that would be impossible under standard vacuum conditions. The comprehensive diagnostic capabilities built into modern systems provide real-time insights into system performance, enabling predictive maintenance that prevents unexpected failures. Return on investment becomes evident through improved yield rates, reduced defect levels, lower operational costs, and enhanced capability to pursue advanced applications that command premium pricing in the marketplace.

Tips And Tricks

How Can Vacuum Technology Improve Process Stability and Output?

29

May

How Can Vacuum Technology Improve Process Stability and Output?

In modern industrial manufacturing, process stability and consistent output are not optional goals — they are operational necessities. vacuum technology has emerged as one of the most reliable engineering tools for achieving both. By removing gas mol...
View More
How Do Vacuum Accessories Support Faster Vacuum System Upgrades?

29

May

How Do Vacuum Accessories Support Faster Vacuum System Upgrades?

When a vacuum system needs to be upgraded, the speed and success of that process depend heavily on more than just the main pump or chamber. The supporting components — the fittings, adapters, flanges, and connectors that link every element of the sys...
View More
Which Vacuum Accessories Improve Industrial Process Reliability Most?

29

May

Which Vacuum Accessories Improve Industrial Process Reliability Most?

In high-demand industrial environments, the performance of a vacuum system is rarely determined by the pump alone. The supporting components — the vacuum accessories that seal, connect, isolate, and protect every part of the system — are what separat...
View More
How Do Custom Vacuum Systems Support Specialized Manufacturing Needs?

29

May

How Do Custom Vacuum Systems Support Specialized Manufacturing Needs?

In today's advanced manufacturing landscape, standard off-the-shelf equipment often falls short when processes demand precision, repeatability, and environmental control that generic solutions simply cannot deliver. custom vacuum systems have emerged...
View More

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

ultra high vacuum solutions

Advanced Multi-Stage Pumping Architecture

Advanced Multi-Stage Pumping Architecture

Ultra high vacuum solutions employ sophisticated multi-stage pumping architectures that systematically remove gases across different pressure ranges for optimal performance. The system typically begins with roughing pumps that reduce pressure from atmospheric levels to moderate vacuum, followed by turbomolecular pumps providing intermediate vacuum stages. Ion pumps and non-evaporable getter pumps then achieve and maintain the ultimate pressure levels. This coordinated approach ensures each pump operates within its optimal efficiency range, maximizing overall system performance while minimizing energy consumption. The intelligent sequencing prevents backstreaming of pump oils and contaminants into the process chamber, maintaining the pristine environment essential for critical applications. Automated valve control manages transitions between pumping stages seamlessly, protecting sensitive equipment from pressure surges. The redundancy built into quality ultra high vacuum solutions provides operational security, allowing maintenance on individual pump components without complete system shutdown. This architecture delivers faster pumpdown times compared to single-stage systems, reducing cycle times and increasing throughput. The modular design facilitates upgrades and expansions as application requirements evolve, protecting your capital investment over decades of operation.
Precision Contamination Management Systems

Precision Contamination Management Systems

Managing contamination at ultra high vacuum levels requires specialized approaches that standard vacuum systems cannot provide. Ultra high vacuum solutions incorporate comprehensive contamination management through multiple integrated mechanisms. High-temperature bakeout capabilities, often reaching 200-400 degrees Celsius, drive absorbed water vapor and hydrocarbons from internal chamber surfaces, achieving base pressures several orders of magnitude lower than unbaked systems. Strategically positioned cold traps and baffles capture residual contaminants before they reach critical process areas, while all-metal sealed construction eliminates elastomer outgassing that compromises vacuum quality. Material selection focuses on low outgassing characteristics, with electropolished stainless steel surfaces minimizing adsorption sites for residual gases. The systems include provisions for in-situ cleaning procedures without breaking vacuum, maintaining productivity while ensuring cleanliness standards. Residual gas analyzers integrated into ultra high vacuum solutions provide real-time compositional analysis of the residual atmosphere, identifying contamination sources and verifying process gas purity. This level of contamination control directly translates into superior product quality for thin films, surface treatments, and analytical procedures where even trace contaminants cause defects or measurement errors. The investment in contamination management pays dividends through higher yields and reproducible results across production runs.
Intelligent Monitoring and Control Integration

Intelligent Monitoring and Control Integration

Modern ultra high vacuum solutions feature comprehensive monitoring and control systems that transform complex vacuum technology into user-friendly, reliable production tools. Advanced pressure measurement incorporates multiple gauge technologies, including cold cathode, hot cathode, and residual gas analyzers, providing accurate readings across the entire vacuum range from atmosphere to extreme low pressure. The integrated control systems continuously monitor dozens of parameters including pump currents, temperatures, valve positions, and gas flow rates, detecting anomalies before they impact processes. Automated sequences handle routine operations such as pumpdown, venting, and backfilling with programmable recipes that ensure consistency across operators and shifts. Remote monitoring capabilities allow supervisors and maintenance teams to track system performance from anywhere, receiving alerts when parameters drift outside acceptable ranges. Data logging creates comprehensive records for quality documentation and process optimization, supporting continuous improvement initiatives. The intuitive human-machine interfaces present complex information clearly, enabling operators to make informed decisions quickly. Integration with facility control systems through standard industrial protocols allows ultra high vacuum solutions to function as intelligent nodes within broader manufacturing execution systems. This connectivity facilitates coordinated operation with upstream and downstream processes, optimizing overall production flow and equipment utilization across your facility.

Have questions about the company?

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000