Vacuum Engineering Solutions - Advanced Systems

All Categories

vacuum engineering solutions

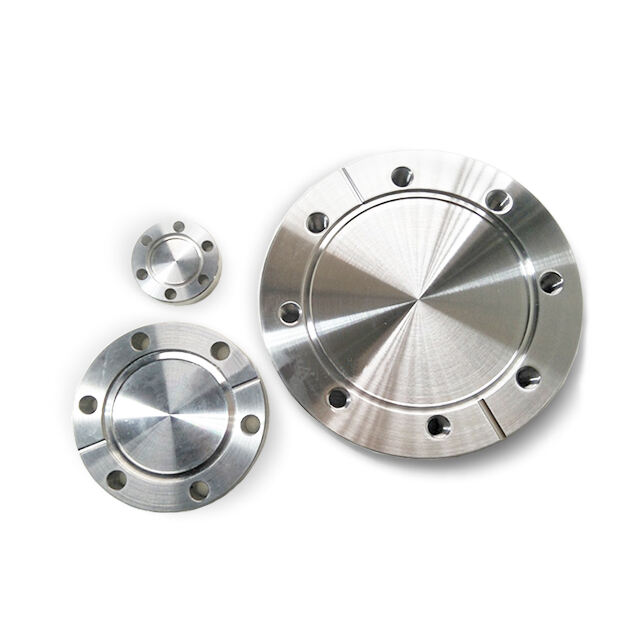
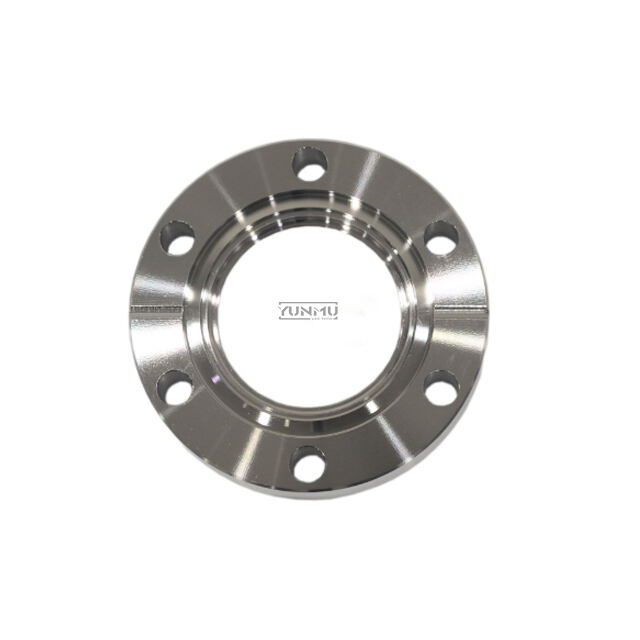
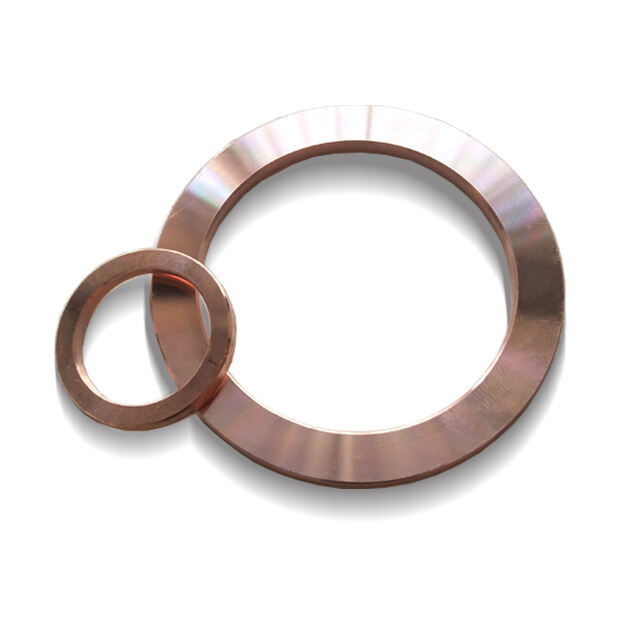
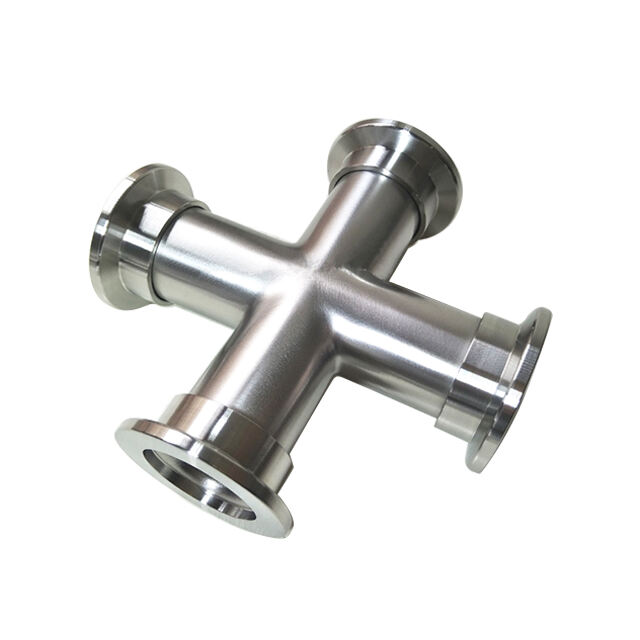
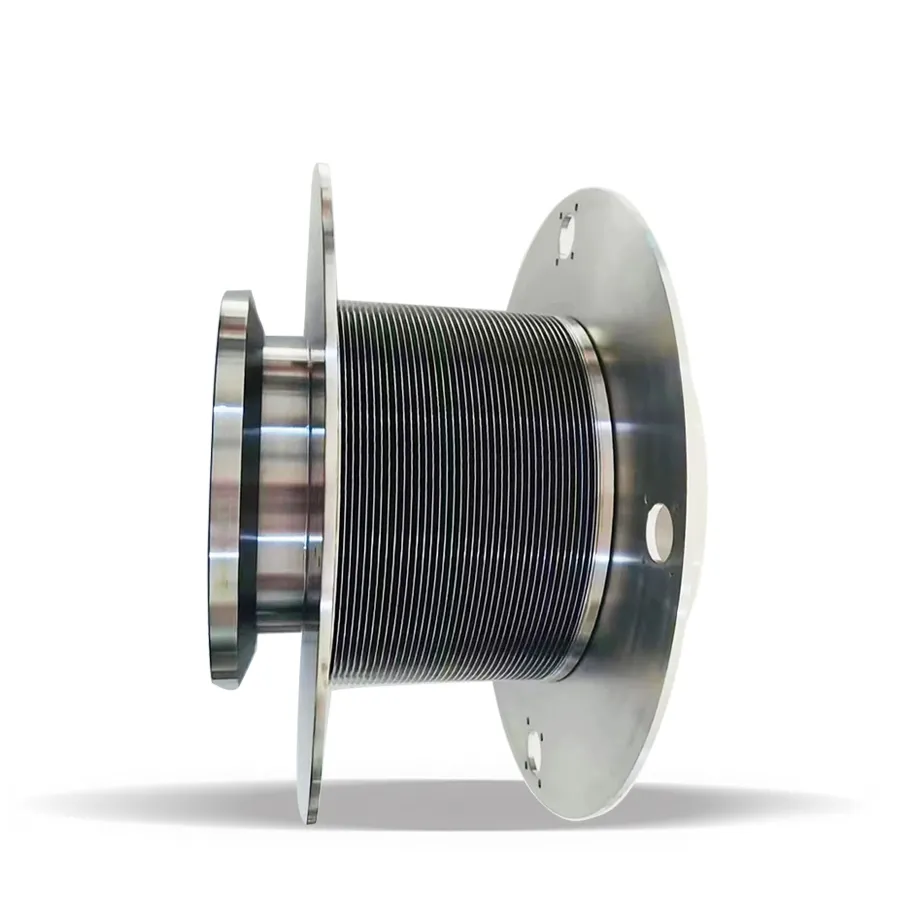
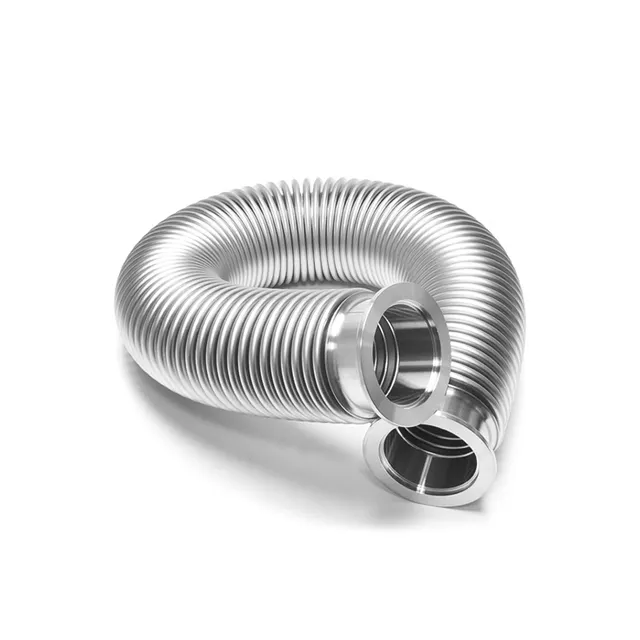
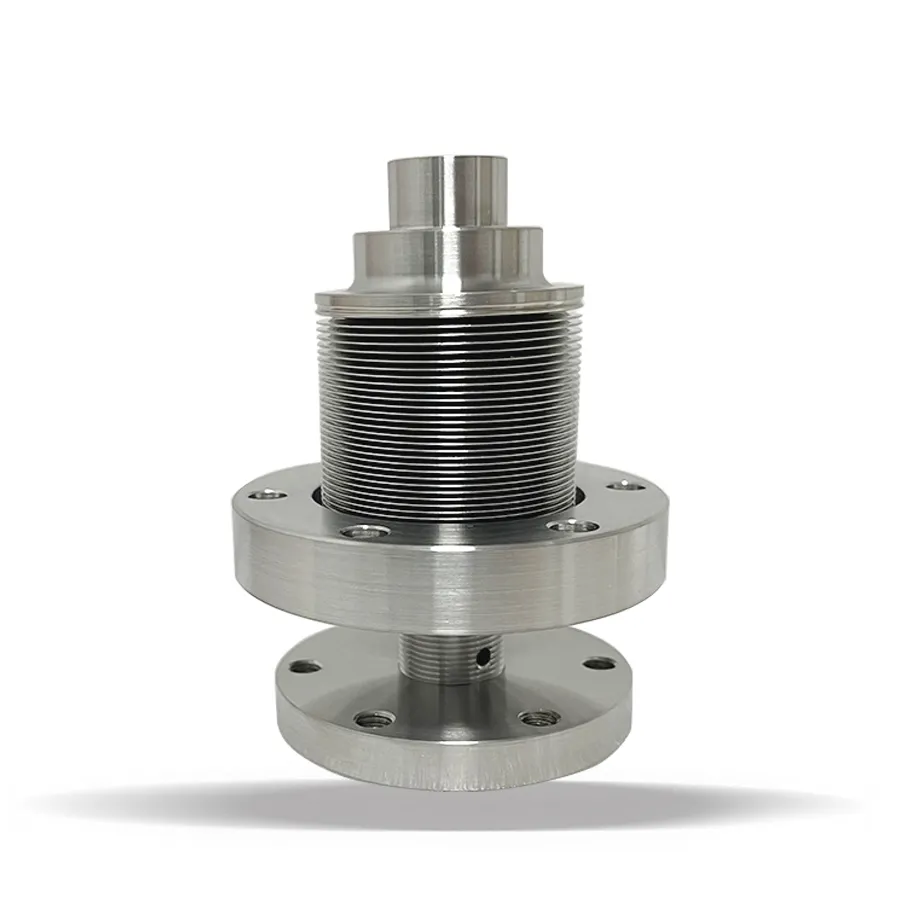
Vacuum engineering solutions represent specialized systems and technologies designed to create, maintain, and control low-pressure environments for industrial and scientific applications. These comprehensive solutions encompass vacuum pumps, chambers, gauges, valves, fittings, and complete turnkey systems that enable precise atmospheric control. Modern vacuum engineering solutions integrate advanced automation, monitoring capabilities, and energy-efficient components to deliver reliable performance across demanding operational conditions. The main functions include evacuating air and gases from sealed chambers, maintaining consistent vacuum levels, preventing contamination, and enabling processes that require controlled low-pressure environments. Technological features of contemporary vacuum engineering solutions include intelligent control systems with real-time monitoring, variable speed drives for energy optimization, leak detection capabilities, and modular designs that allow customization for specific applications. These solutions employ various vacuum generation technologies such as rotary vane pumps, dry screw pumps, turbomolecular pumps, and diffusion pumps, each suited to different pressure ranges and process requirements. Applications span numerous industries including semiconductor manufacturing, pharmaceutical production, food packaging, metallurgy, coating processes, scientific research, and aerospace testing. In semiconductor fabrication, vacuum engineering solutions enable thin-film deposition and etching processes. Pharmaceutical companies utilize these systems for freeze-drying medications and sterile packaging. Food processors depend on vacuum technology for extended shelf-life packaging, while metallurgical operations use vacuum furnaces for heat treatment and degassing. The versatility and precision of vacuum engineering solutions make them indispensable for modern manufacturing and research facilities seeking to optimize production quality, reduce contamination risks, and achieve superior process control in controlled atmospheric environments.

Popular Products

Investing in professional vacuum engineering solutions delivers substantial operational benefits that directly impact your bottom line and production capabilities. These systems significantly reduce energy consumption through intelligent controls that adjust pump speeds based on actual demand, cutting utility costs by up to forty percent compared to traditional fixed-speed systems. You gain consistent product quality because vacuum engineering solutions maintain precise pressure levels throughout production cycles, eliminating variations that cause defects and waste. The advanced monitoring capabilities alert operators to potential issues before they escalate into costly downtime, enabling proactive maintenance scheduling that keeps your operations running smoothly. Your facility benefits from reduced contamination risks as vacuum engineering solutions create clean, controlled environments that protect sensitive products from airborne particles and moisture. This protection proves especially valuable in pharmaceutical, electronics, and food processing applications where product purity determines marketability and regulatory compliance. The modular design of modern vacuum engineering solutions allows you to scale capacity as your business grows, protecting your initial investment while accommodating expansion without complete system replacement. You experience faster processing times because optimized vacuum systems reach target pressures quickly and maintain stability, increasing throughput and production efficiency. These solutions also extend equipment lifespan through gentle, controlled operation that reduces mechanical stress on components. Environmental compliance becomes easier as vacuum engineering solutions minimize emissions and support sustainable manufacturing practices, helping you meet regulatory requirements and corporate sustainability goals. The comprehensive support typically available with professional vacuum engineering solutions includes installation guidance, operator training, and ongoing technical assistance, ensuring your team maximizes system performance. Decision-makers appreciate the clear return on investment through reduced operating costs, improved yield rates, decreased maintenance expenses, and enhanced production flexibility that vacuum engineering solutions provide across diverse industrial applications.

Tips And Tricks

How Can Vacuum Technology Improve Process Stability and Output?

29

May

How Can Vacuum Technology Improve Process Stability and Output?

In modern industrial manufacturing, process stability and consistent output are not optional goals — they are operational necessities. vacuum technology has emerged as one of the most reliable engineering tools for achieving both. By removing gas mol...
View More
Why Is Vacuum Chamber Design Important for Industrial Applications?

29

May

Why Is Vacuum Chamber Design Important for Industrial Applications?

In industrial manufacturing and research environments, the vacuum chamber is far more than a sealed metal enclosure. It is a precisely engineered system whose design directly determines whether a process succeeds or fails. From semiconductor fabricat...
View More
What Should Buyers Know Before Choosing a Vacuum Chamber Supplier?

29

May

What Should Buyers Know Before Choosing a Vacuum Chamber Supplier?

Selecting the right supplier for a vacuum chamber is one of the most consequential procurement decisions an industrial buyer can make. Whether you are sourcing for research and development, manufacturing, food processing, or aerospace testing, the qu...
View More
How Can Edge Welded Bellow Systems Improve Vacuum Performance?

04

Jun

How Can Edge Welded Bellow Systems Improve Vacuum Performance?

In high-precision vacuum environments, even the smallest mechanical compromise can lead to significant performance degradation. The edge welded bellow has emerged as one of the most reliable solutions for maintaining vacuum integrity while accommodat...
View More

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

vacuum engineering solutions

Advanced Automation and Intelligent Control Systems

Advanced Automation and Intelligent Control Systems

Modern vacuum engineering solutions incorporate sophisticated automation technologies that transform operational efficiency and process reliability. These intelligent control systems feature programmable logic controllers with intuitive human-machine interfaces that simplify operation while providing comprehensive process oversight. Operators can establish custom vacuum profiles tailored to specific production requirements, with the system automatically adjusting pump speeds, valve positions, and cycle times to maintain optimal conditions. Real-time data logging captures pressure trends, cycle durations, and system performance metrics that support quality documentation and continuous improvement initiatives. The predictive maintenance algorithms analyze operational patterns to forecast component wear and schedule service interventions before failures occur, dramatically reducing unexpected downtime. Remote monitoring capabilities enable technical teams to assess system status from any location, facilitating rapid troubleshooting and expert support without site visits. Integration with existing plant automation systems through standard industrial protocols allows vacuum engineering solutions to communicate seamlessly with upstream and downstream equipment, creating coordinated production workflows. Alarm management features prioritize notifications based on severity, ensuring operators focus attention where needed most. These advanced control capabilities not only enhance day-to-day operations but also provide the detailed process documentation increasingly required for regulatory compliance and quality certifications across regulated industries.
Energy-Efficient Operation and Sustainability Benefits

Energy-Efficient Operation and Sustainability Benefits

Contemporary vacuum engineering solutions prioritize energy efficiency through innovative technologies that substantially reduce power consumption while maintaining superior performance. Variable frequency drives adjust motor speeds precisely to match process requirements rather than running continuously at full capacity, eliminating the energy waste inherent in traditional on-off cycling systems. Heat recovery options capture thermal energy from pump cooling systems for reuse in facility heating applications, further improving overall energy utilization. The implementation of dry pump technologies in vacuum engineering solutions eliminates the need for operating fluids, removing disposal costs and environmental concerns associated with contaminated oils while reducing maintenance requirements. Optimized system designs minimize pressure drops through properly sized piping and strategically placed components, allowing pumps to achieve target vacuum levels with less energy input. Standby modes automatically reduce power consumption during idle periods without compromising response times when production resumes. These energy-saving features translate directly into lower operating costs that accumulate substantially over system lifespans. Beyond economic advantages, the reduced energy consumption and elimination of process fluids position vacuum engineering solutions as environmentally responsible choices that support corporate sustainability commitments. Facilities pursuing green building certifications or carbon footprint reduction goals find these systems valuable contributors to environmental performance targets while simultaneously improving operational economics through decreased utility consumption and waste generation.
Application Versatility and Customization Capabilities

Application Versatility and Customization Capabilities

The exceptional adaptability of vacuum engineering solutions addresses diverse industrial requirements through flexible configurations and customizable components. Modular architectures allow system designers to combine vacuum pumps, chambers, instrumentation, and controls in configurations precisely matched to specific process needs, whether simple single-chamber setups or complex multi-stage production lines. This customization extends to material selection, with options including stainless steel, aluminum, and specialized coatings that resist corrosive environments or meet stringent cleanliness standards for pharmaceutical and food applications. Vacuum engineering solutions accommodate pressure ranges from rough vacuum for packaging applications to ultra-high vacuum for semiconductor processes, with appropriate pump technologies selected for each requirement. The systems integrate seamlessly with specialized process equipment such as coating chambers, freeze dryers, distillation apparatus, and heat treatment furnaces, providing the precise atmospheric control these applications demand. Scalable designs support both pilot-scale research installations and full production systems, allowing organizations to validate processes before committing to large-scale implementation. Quick-change tooling and chamber designs facilitate rapid product changeovers, maximizing equipment utilization across varied production schedules. This versatility ensures vacuum engineering solutions deliver value across pharmaceutical manufacturing, electronics production, food processing, metallurgical operations, scientific research, and numerous other applications, making them strategic investments that adapt as business needs evolve rather than obsolete single-purpose equipment.

Have questions about the company?

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000