Advanced Vacuum Technology Solutions & Systems

All Categories

advanced vacuum technology

Advanced vacuum technology represents a cutting-edge solution designed to create and maintain ultra-low pressure environments for diverse industrial and scientific applications. This sophisticated system combines precision engineering with intelligent control mechanisms to achieve optimal vacuum conditions ranging from low to ultra-high vacuum levels. The main functions include rapid evacuation of air and gases from sealed chambers, precise pressure regulation, contamination prevention, and consistent vacuum maintenance over extended operational periods. Advanced vacuum technology incorporates multi-stage pumping systems, automated monitoring capabilities, and energy-efficient components that work seamlessly together. Technological features include digital pressure sensors with real-time feedback, variable speed drive motors for adaptive performance, advanced sealing materials that minimize leakage, and integrated safety protocols to protect both equipment and operators. The systems utilize innovative pump designs such as turbomolecular, dry scroll, and ion pumps depending on specific requirements. Applications span semiconductor manufacturing where particle-free environments are critical, pharmaceutical production requiring sterile processing conditions, research laboratories conducting material science experiments, aerospace component testing, vacuum coating and metallization processes, electron microscopy, mass spectrometry, and food packaging industries. Advanced vacuum technology serves as an essential infrastructure component across manufacturing facilities, enabling processes that would be impossible under atmospheric conditions while delivering reliability and precision that modern production demands.

New Products

Implementing advanced vacuum technology delivers substantial operational benefits that directly impact your bottom line and production quality. Energy efficiency stands as a primary advantage, with modern systems consuming significantly less power compared to traditional vacuum equipment through intelligent motor control and optimized pump cycling. You will experience faster process times as advanced vacuum technology achieves target pressure levels more quickly, reducing cycle duration and increasing throughput capacity. The enhanced reliability translates to fewer unexpected breakdowns and lower maintenance costs, keeping your operations running smoothly with minimal downtime. Product quality improvements become immediately noticeable as contamination risks decrease dramatically, ensuring cleaner processing environments that meet stringent industry standards. These systems adapt to varying production demands through programmable controls, allowing you to customize vacuum profiles for different applications without equipment changes. Cost savings accumulate through reduced consumable replacement frequency, extended component lifespan, and lower energy bills month after month. Operational flexibility increases as advanced vacuum technology handles multiple process requirements within a single system, eliminating the need for separate dedicated equipment. User-friendly interfaces simplify training requirements and reduce operator errors, while comprehensive diagnostic capabilities enable predictive maintenance scheduling. Environmental compliance becomes easier to achieve as modern vacuum systems produce fewer emissions and support sustainable manufacturing practices. The precision control capabilities ensure consistent results across production batches, reducing waste and improving yield rates. Investment in advanced vacuum technology positions your facility for future expansion, with scalable systems that grow alongside your business needs while maintaining performance standards that satisfy demanding quality requirements.

Latest News

Why Are High Quality Vacuum Fittings Critical for Industrial Systems?

29

May

Why Are High Quality Vacuum Fittings Critical for Industrial Systems?

In industrial environments where precision and reliability are non-negotiable, the integrity of every component in a vacuum system determines whether operations succeed or fail. Among all the components that make up a vacuum assembly, vacuum fittings...
View More
Why Is Vacuum Chamber Design Important for Industrial Applications?

29

May

Why Is Vacuum Chamber Design Important for Industrial Applications?

In industrial manufacturing and research environments, the vacuum chamber is far more than a sealed metal enclosure. It is a precisely engineered system whose design directly determines whether a process succeeds or fails. From semiconductor fabricat...
View More
How Can Custom Vacuum Systems Improve Industrial Workflow Stability?

29

May

How Can Custom Vacuum Systems Improve Industrial Workflow Stability?

Industrial workflow stability is one of the most critical factors separating high-performing facilities from those that struggle with downtime, inconsistent output, and rising operational costs. When vacuum technology is involved in production, the p...
View More
Why Are Precision Vacuum Components Important for Industrial Use?

05

Jun

Why Are Precision Vacuum Components Important for Industrial Use?

In high-performance industrial environments, the reliability of every individual part determines the integrity of the entire system. vacuum components are among the most critical elements in this equation, forming the backbone of systems that depend ...
View More

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

advanced vacuum technology

Intelligent Pressure Control Systems

Intelligent Pressure Control Systems

Advanced vacuum technology features sophisticated pressure control systems that automatically adjust pumping speed and valve positions to maintain precise vacuum levels throughout your processes. These intelligent systems utilize multiple high-accuracy sensors positioned strategically within vacuum chambers to continuously monitor pressure fluctuations and respond instantaneously to changing conditions. The adaptive algorithms learn your specific process patterns over time, optimizing performance parameters to deliver consistent results while minimizing energy consumption. Real-time data visualization through intuitive touchscreen interfaces allows operators to monitor system status at a glance and make informed adjustments when needed. The control systems integrate seamlessly with existing facility automation networks, enabling remote monitoring and centralized management across multiple vacuum stations. Automated leak detection capabilities identify potential issues before they impact production, triggering alerts and initiating corrective actions to maintain optimal vacuum integrity. This level of precision control eliminates the guesswork associated with manual vacuum regulation, ensuring that every production cycle meets exact specifications while reducing the skill level required for effective operation and maximizing overall equipment effectiveness.
Multi-Stage Pumping Architecture

Multi-Stage Pumping Architecture

The multi-stage pumping architecture employed in advanced vacuum technology combines different pump types in optimized configurations to achieve superior performance across the entire vacuum range. Primary roughing pumps rapidly remove bulk gases from chambers, while secondary high-vacuum pumps take over to reach ultra-low pressure levels efficiently. This staged approach dramatically reduces the time required to achieve working vacuum conditions compared to single-pump systems, directly increasing production capacity. Each pump stage operates at its optimal efficiency point, minimizing energy waste and thermal loading that can affect sensitive processes. Advanced vacuum technology incorporates dry pump options that eliminate oil contamination risks entirely, critical for pharmaceutical, food processing, and semiconductor applications where purity requirements are non-negotiable. The modular design allows for pump combination customization based on your specific vacuum requirements, chamber volumes, and process gas compositions. Redundant pumping capabilities can be integrated for mission-critical applications, ensuring continuous operation even during maintenance activities or component failures. Intelligent pump sequencing extends component lifespan by distributing operational hours evenly across available pumps while sophisticated vibration isolation systems protect sensitive equipment from mechanical disturbances generated during pumping operations.
Advanced Sealing and Materials Technology

Advanced Sealing and Materials Technology

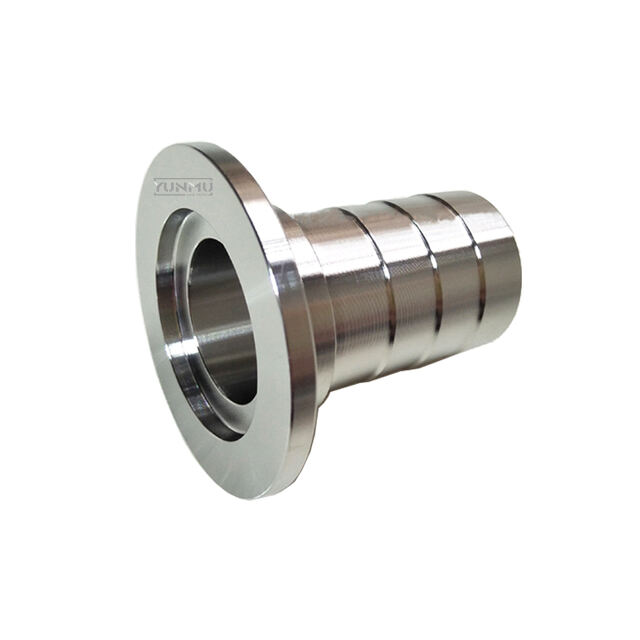
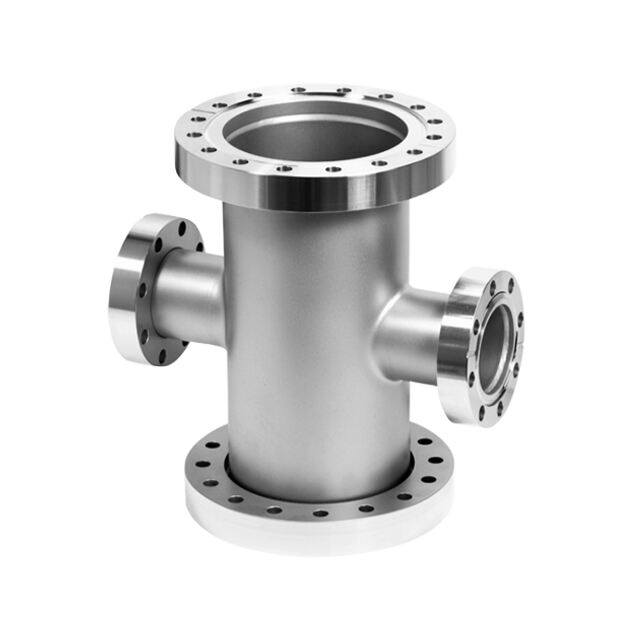
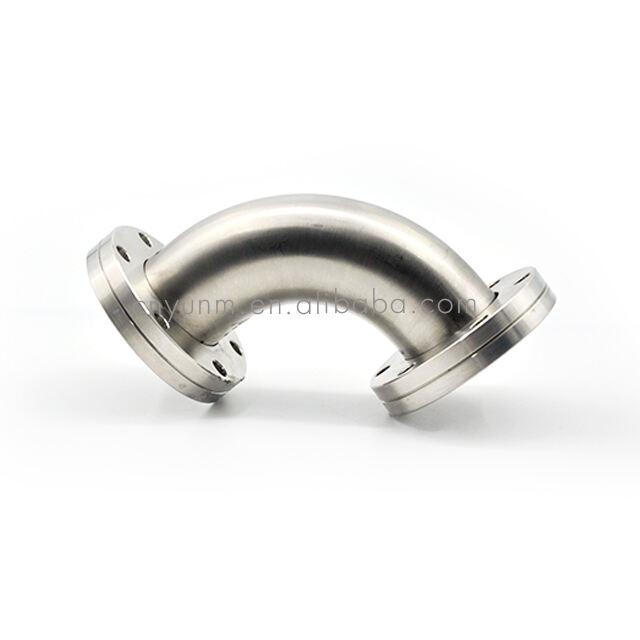
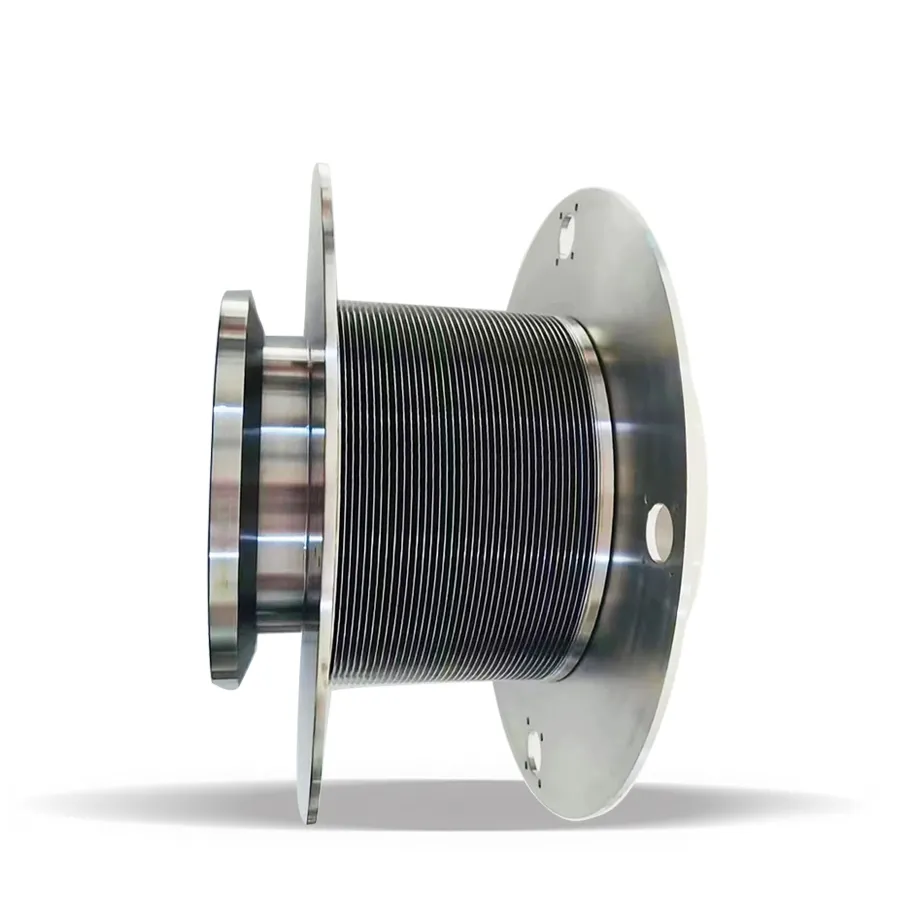
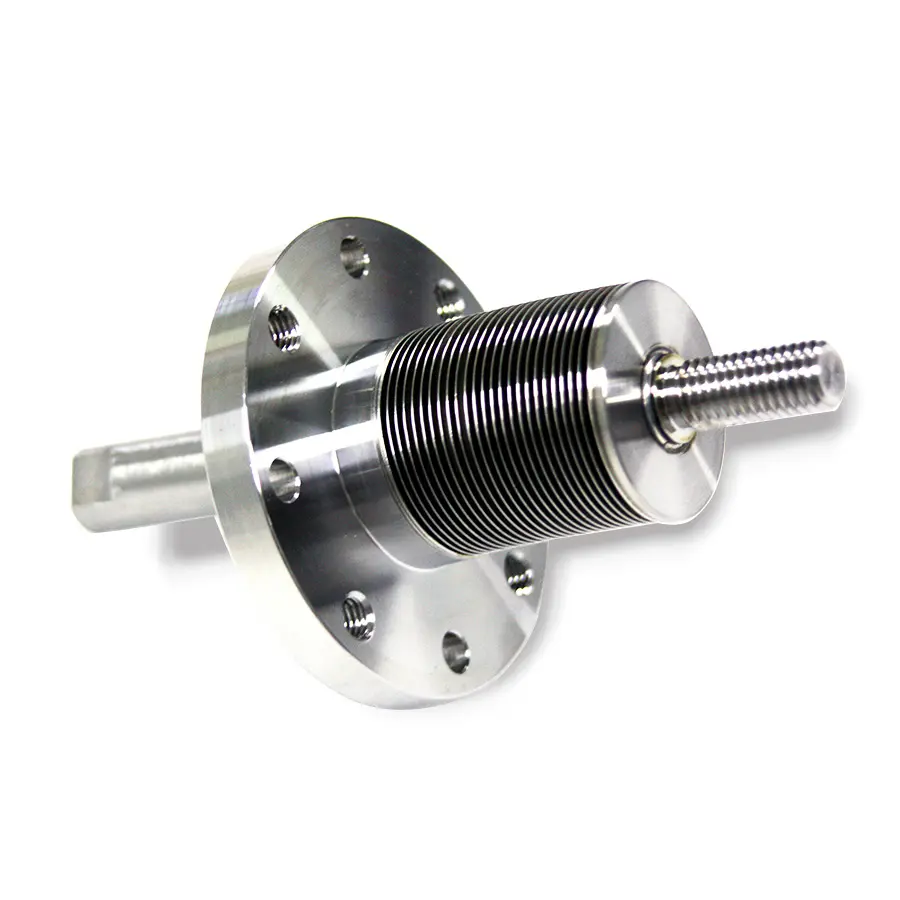
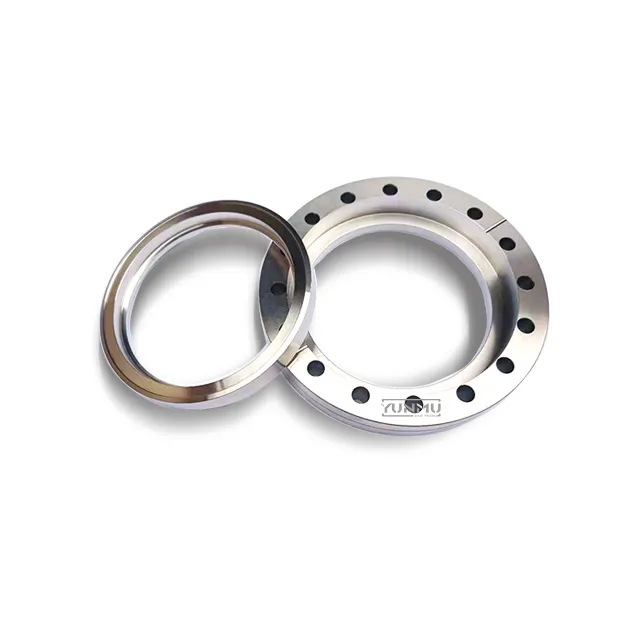
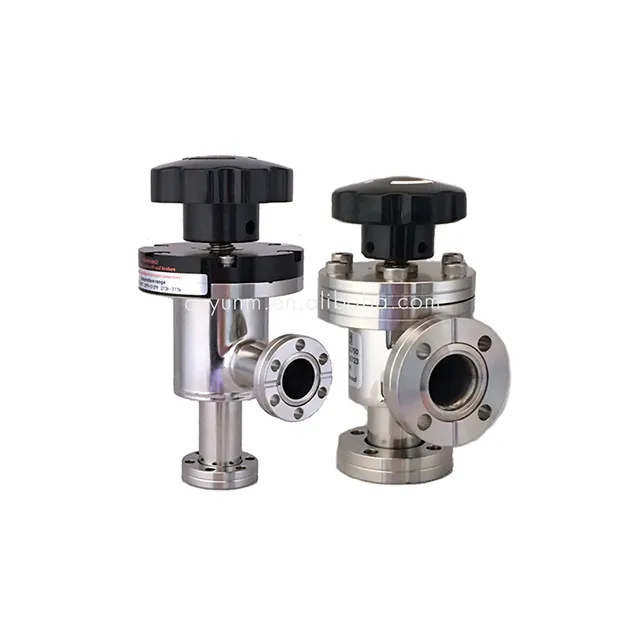
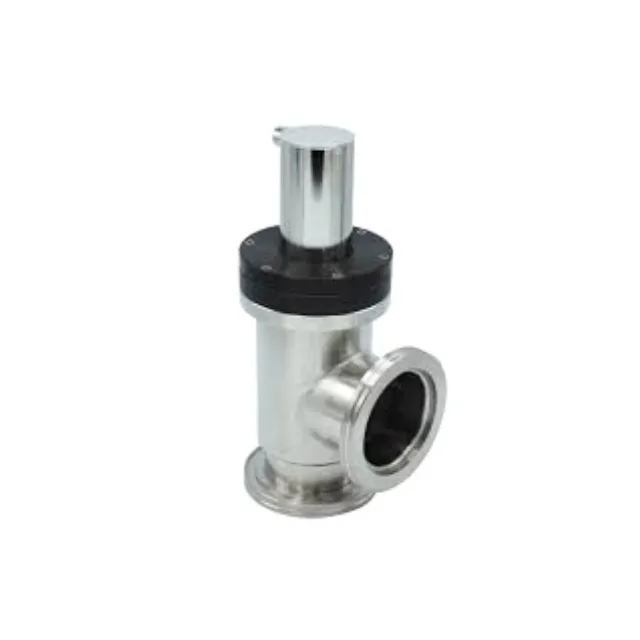
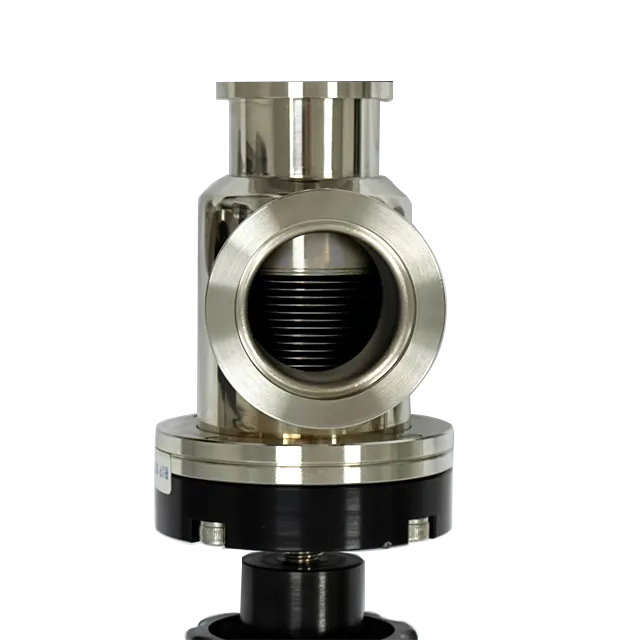
Advanced vacuum technology incorporates breakthrough sealing solutions and specialized materials engineered specifically for demanding vacuum applications, ensuring leak-tight performance that maintains process integrity over extended operational periods. High-performance elastomers and metal seals provide exceptional sealing capabilities across wide temperature ranges while resisting chemical attack from aggressive process gases and cleaning agents. Chamber construction utilizes low-outgassing materials that minimize contamination from internal surfaces, crucial for achieving and maintaining ultra-high vacuum conditions required in research and advanced manufacturing environments. Specialized surface treatments and electropolishing techniques create ultra-smooth internal finishes that facilitate cleaning procedures and reduce particle generation during operation. Conflat flanges and other precision-engineered connection systems ensure reliable, repeatable sealing at every joint and interface point throughout the vacuum system. The materials selected for advanced vacuum technology demonstrate excellent thermal stability, preventing dimensional changes that could compromise seal integrity during temperature cycling or high-temperature bakeout procedures. Corrosion-resistant alloys extend system lifespan even when processing corrosive gases or operating in harsh industrial environments. These advanced materials and sealing technologies work together to minimize virtual leaks, reduce pumping requirements, and maintain vacuum quality that meets the most stringent application specifications while reducing maintenance frequency and associated costs.

Have questions about the company?

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000