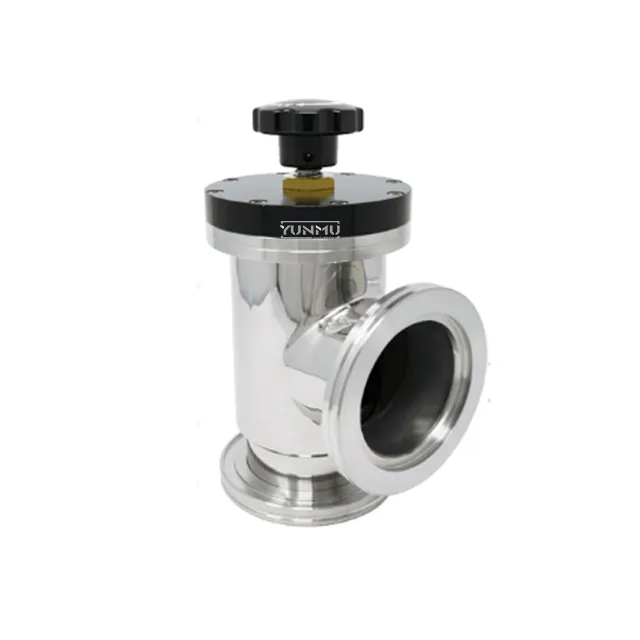
Industrial Vacuum Technology Solutions & Benefits

All Categories

industrial vacuum technology

Industrial vacuum technology represents a critical advancement in modern manufacturing and processing environments, delivering powerful suction capabilities designed to handle demanding material handling, cleaning, and containment tasks across diverse sectors. This sophisticated technology employs high-performance vacuum systems engineered to remove dust, debris, liquids, and hazardous materials from production areas, ensuring workplace safety and operational efficiency. Industrial vacuum technology integrates robust motors, advanced filtration mechanisms, and durable construction materials to withstand continuous operation in challenging conditions. The main functions include material recovery, surface preparation, spill cleanup, and maintaining contamination-free environments essential for quality production standards. Technological features encompass variable suction control, HEPA filtration options, explosion-proof designs for volatile environments, and modular configurations adaptable to specific operational requirements. These systems range from portable units for localized cleaning to centralized installations serving entire facilities. Applications span pharmaceutical manufacturing, food processing, metalworking, chemical plants, automotive production, and electronics assembly where precise cleanliness standards are mandatory. Industrial vacuum technology supports compliance with environmental regulations and occupational health standards by effectively capturing airborne particulates and preventing material cross-contamination. The technology continuously evolves with innovations in energy efficiency, noise reduction, and smart monitoring capabilities that provide real-time performance data. Organizations implementing industrial vacuum technology experience measurable improvements in production quality, worker safety, and operational cleanliness while reducing manual labor requirements and minimizing environmental impact through controlled material handling and disposal processes.

New Products

Implementing industrial vacuum technology delivers substantial cost savings by reducing manual cleaning labor and minimizing production downtime caused by contamination issues. These systems operate continuously with minimal supervision, allowing your workforce to focus on value-adding activities rather than repetitive cleaning tasks. The technology significantly enhances workplace safety by immediately removing hazardous materials, combustible dust, and toxic substances that pose health risks to employees and fire hazards to facilities. You gain improved product quality as industrial vacuum technology maintains contamination-free production environments, preventing defects caused by foreign particles and ensuring consistent output that meets stringent quality specifications. Energy-efficient designs reduce operational expenses through optimized motor performance and intelligent suction control that adjusts power consumption based on actual workload demands. The versatility of industrial vacuum technology allows seamless integration into existing production workflows across multiple applications, from fine powder recovery to heavy debris removal, providing flexibility as your operational needs evolve. Maintenance requirements remain straightforward with accessible filter replacement, simplified component servicing, and durable construction that extends equipment lifespan and maximizes return on investment. Environmental compliance becomes manageable as these systems capture and contain materials that would otherwise become airborne pollutants or waste disposal challenges, helping you meet regulatory standards while demonstrating corporate responsibility. The technology adapts to various industry requirements with specialized configurations including explosion-proof certifications, cleanroom compatibility, and corrosion-resistant materials for chemical environments. Real-time monitoring capabilities available in advanced industrial vacuum technology systems provide operational insights that enable predictive maintenance, prevent unexpected failures, and optimize performance efficiency. Organizations experience faster cleaning cycles, reduced material waste through effective recovery systems, and improved facility aesthetics that positively impact employee morale and client perceptions during site visits.

Latest News

Why Are Stainless Steel Vacuum Fittings Preferred in Harsh Environments?

29

May

Why Are Stainless Steel Vacuum Fittings Preferred in Harsh Environments?

In industrial and scientific settings where reliability is non-negotiable, the choice of vacuum fittings can determine whether a system performs flawlessly or fails under pressure. Stainless steel has emerged as the dominant material for vacuum fitti...
View More
Why Is Vacuum Chamber Design Important for Industrial Applications?

29

May

Why Is Vacuum Chamber Design Important for Industrial Applications?

In industrial manufacturing and research environments, the vacuum chamber is far more than a sealed metal enclosure. It is a precisely engineered system whose design directly determines whether a process succeeds or fails. From semiconductor fabricat...
View More
Can Custom Vacuum Systems Reduce Long Term Operational Challenges?

29

May

Can Custom Vacuum Systems Reduce Long Term Operational Challenges?

Across manufacturing, research, and industrial processing environments, operational challenges tend to compound over time. Equipment that was selected for general use often reveals its limitations as production demands shift, process tolerances tight...
View More
Why Are Integrated Vacuum Solutions Important for Modern Factories?

04

Jun

Why Are Integrated Vacuum Solutions Important for Modern Factories?

Modern manufacturing environments are under constant pressure to improve efficiency, reduce contamination risks, and maintain precise process control across every production stage. In this context, vacuum solutions have evolved from being a periphera...
View More

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

industrial vacuum technology

Advanced Filtration Systems Ensure Superior Air Quality

Advanced Filtration Systems Ensure Superior Air Quality

Industrial vacuum technology incorporates multi-stage filtration systems that capture particles ranging from large debris to microscopic contaminants as small as 0.3 microns, delivering exceptional air purification essential for sensitive manufacturing environments. HEPA and ULPA filtration options provide 99.97% to 99.999% particle removal efficiency, protecting both workers and products from harmful exposure while maintaining negative pressure containment. The filtration technology prevents filter clogging through automatic cleaning mechanisms including pulse-jet systems and mechanical shakers that extend filter life and maintain consistent suction performance throughout operation. Specialized filter media options accommodate specific materials such as oily mists, explosive dusts, and chemically reactive substances, ensuring safe capture and containment. This advanced filtration capability within industrial vacuum technology eliminates the need for frequent filter replacements, reducing maintenance costs and operational interruptions. The systems effectively separate recovered materials for recycling or proper disposal, supporting sustainability initiatives while preventing valuable materials from becoming waste. By maintaining superior indoor air quality, these filtration systems help organizations comply with OSHA standards and create healthier work environments that reduce employee sick leave and improve productivity across all shifts.
Robust Construction Delivers Reliable Performance in Harsh Environments

Robust Construction Delivers Reliable Performance in Harsh Environments

Industrial vacuum technology features heavy-duty construction using corrosion-resistant stainless steel, reinforced polymers, and industrial-grade components engineered to withstand abrasive materials, chemical exposure, and continuous operation in demanding production settings. The rugged design includes reinforced hose assemblies, impact-resistant collection containers, and sealed motor housings that prevent material infiltration and extend equipment lifespan significantly beyond consumer-grade alternatives. Thermal protection systems prevent motor overheating during extended operation, while vibration dampening mounting reduces structural stress and operational noise levels. This durability ensures industrial vacuum technology maintains consistent performance across multiple shifts without degradation, providing reliable material handling regardless of environmental challenges. The robust construction supports mobile applications with heavy-duty casters and ergonomic handles for easy repositioning, while stationary installations feature secure mounting systems for permanent integration into production lines. Manufacturers engineer these systems to handle temperature extremes, moisture exposure, and physical impacts common in industrial settings, minimizing unplanned downtime and repair costs. The investment in quality construction pays dividends through reduced total cost of ownership, fewer replacement cycles, and consistent performance that supports uninterrupted production schedules essential for meeting customer commitments and maintaining competitive advantages in demanding markets.
Customizable Configurations Adapt to Specific Operational Needs

Customizable Configurations Adapt to Specific Operational Needs

Industrial vacuum technology offers extensive customization options that align precisely with unique operational requirements, facility layouts, and material handling challenges across diverse industries and applications. Modular designs allow configuration of suction power, collection capacity, filtration specifications, and accessory tools to match specific tasks ranging from fine powder recovery to large debris removal. Organizations can specify explosion-proof certifications for combustible dust environments, cleanroom-compatible designs for pharmaceutical applications, or chemical-resistant materials for corrosive substance handling. The technology supports both centralized systems serving multiple workstations through networked piping and portable units for flexible deployment across changing work areas. Variable frequency drives enable precise suction control, optimizing energy consumption while providing appropriate power for different materials and distances. Accessory options include specialized nozzles for confined spaces, conductive hoses for static-sensitive environments, and automated material discharge systems for continuous operation. This customization capability ensures industrial vacuum technology integrates seamlessly into existing workflows without requiring significant facility modifications or process changes. Organizations benefit from scalable solutions that grow with expanding operations, adding capacity and capabilities as production demands increase. The ability to tailor industrial vacuum technology to specific applications maximizes effectiveness, prevents over-investment in unnecessary features, and ensures optimal performance for the unique challenges each facility faces in maintaining cleanliness, safety, and operational efficiency.

Have questions about the company?

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000